
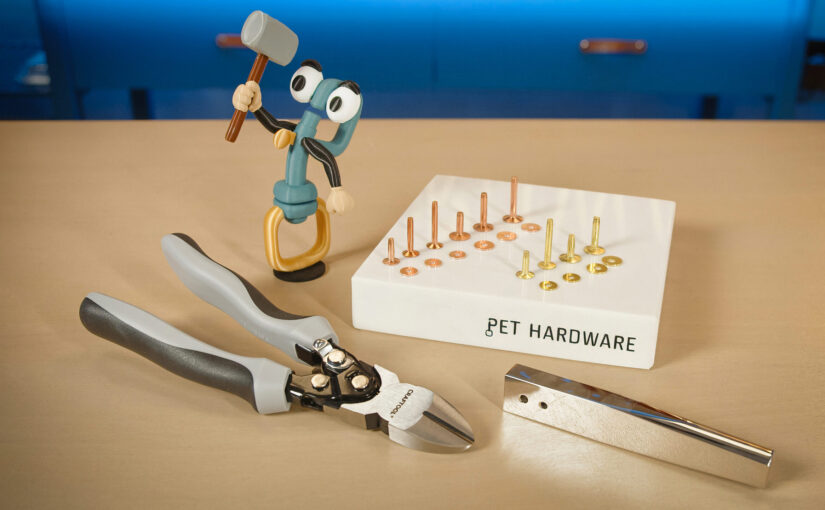
Copper and brass rivets with burrs make some of the strongest joints in saddlery. You use them mainly where a rivet has to hold well, where the joint will be under stress, or where the rivet should also be a visible handcrafted detail. You will find them on leather dog collars, leashes, harnesses, belts, bags and other leather goods, where besides adding strength they can also play a distinct design role.
Unlike ordinary double cap rivets, they involve more than choosing the right rivet size: you also deal with the shank length, seating the burr and then peening the end. That is why they deserve a guide of their own.
In this article, we look at how copper and brass rivets with burrs work, how to choose the right size, what tools you need and how to set them step by step.
How a rivet and burr work
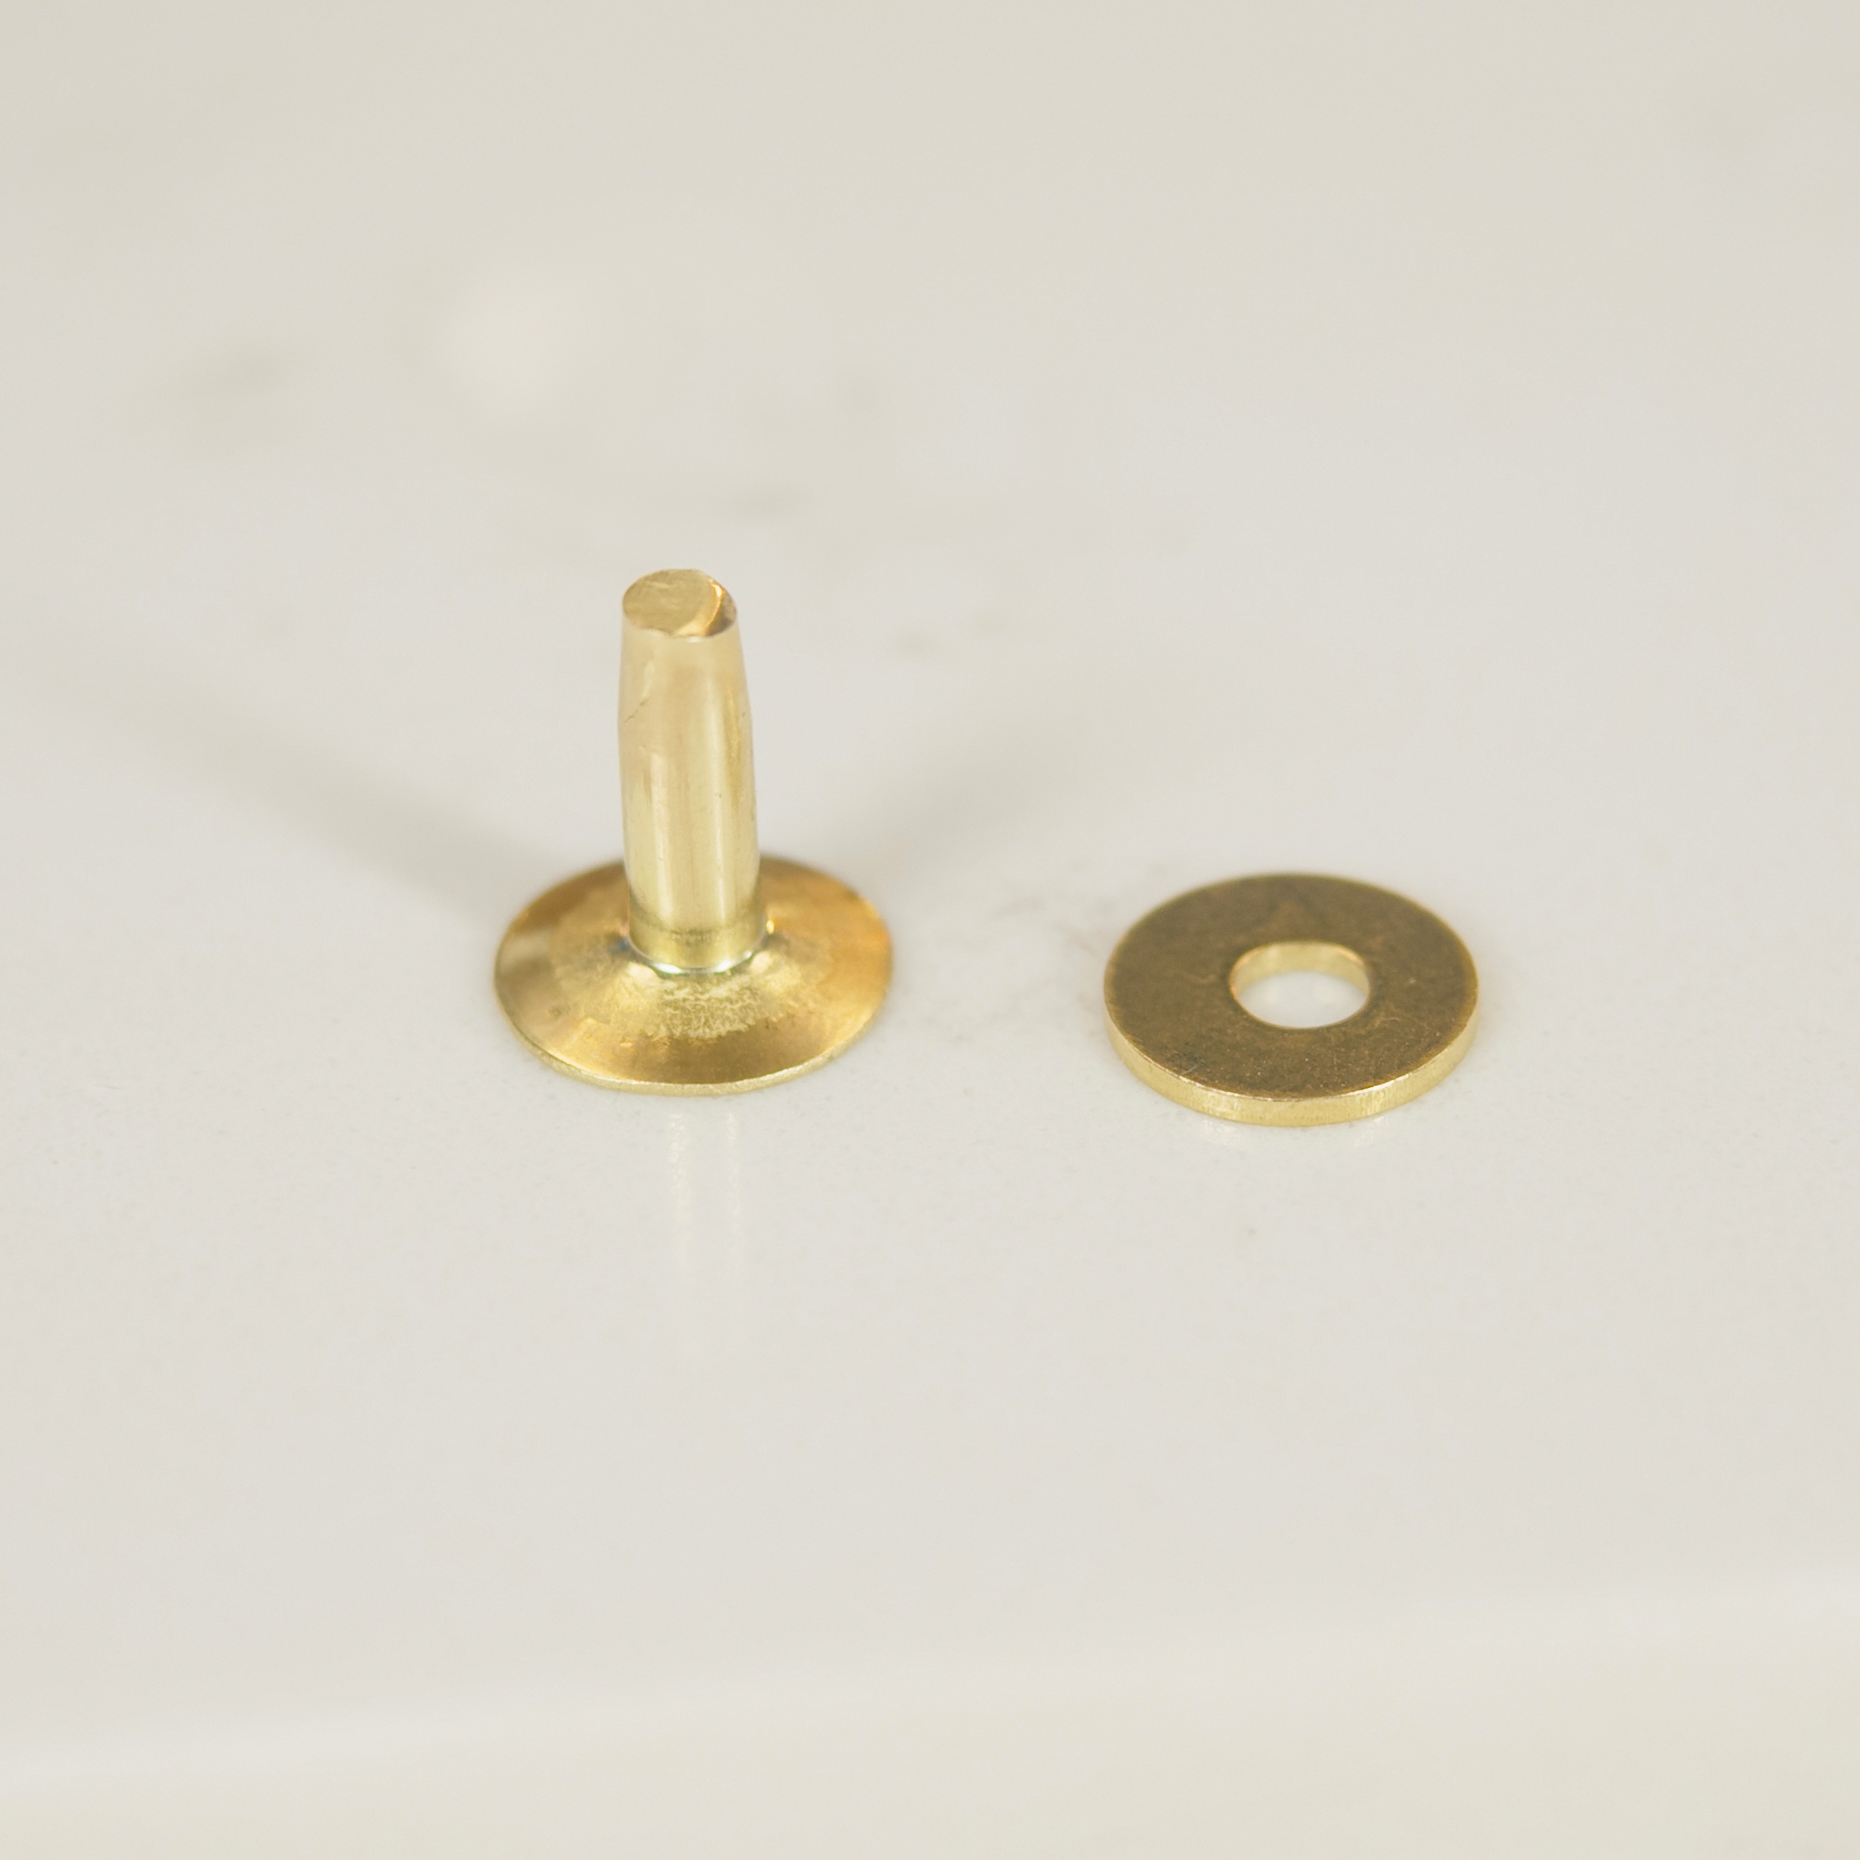
Copper and brass rivets with burrs consist of two parts: the rivet with its shank and a separate burr (washer). You push the shank through a prepared hole in the material, slip the burr over it from the other side and drive the burr down against the material with a rivet setter.
Then you nip off the excess shank and peen the rest into the final rivet head. The result is a strong, permanent joint.
Working with the burr, the shank length and peening the end are what set this type of rivet apart from more common saddlery rivets.
Copper or brass: which one to choose
Copper and brass rivets with burrs work on the same principle. The difference lies mainly in the material, the look and the effect they will have on the finished piece.
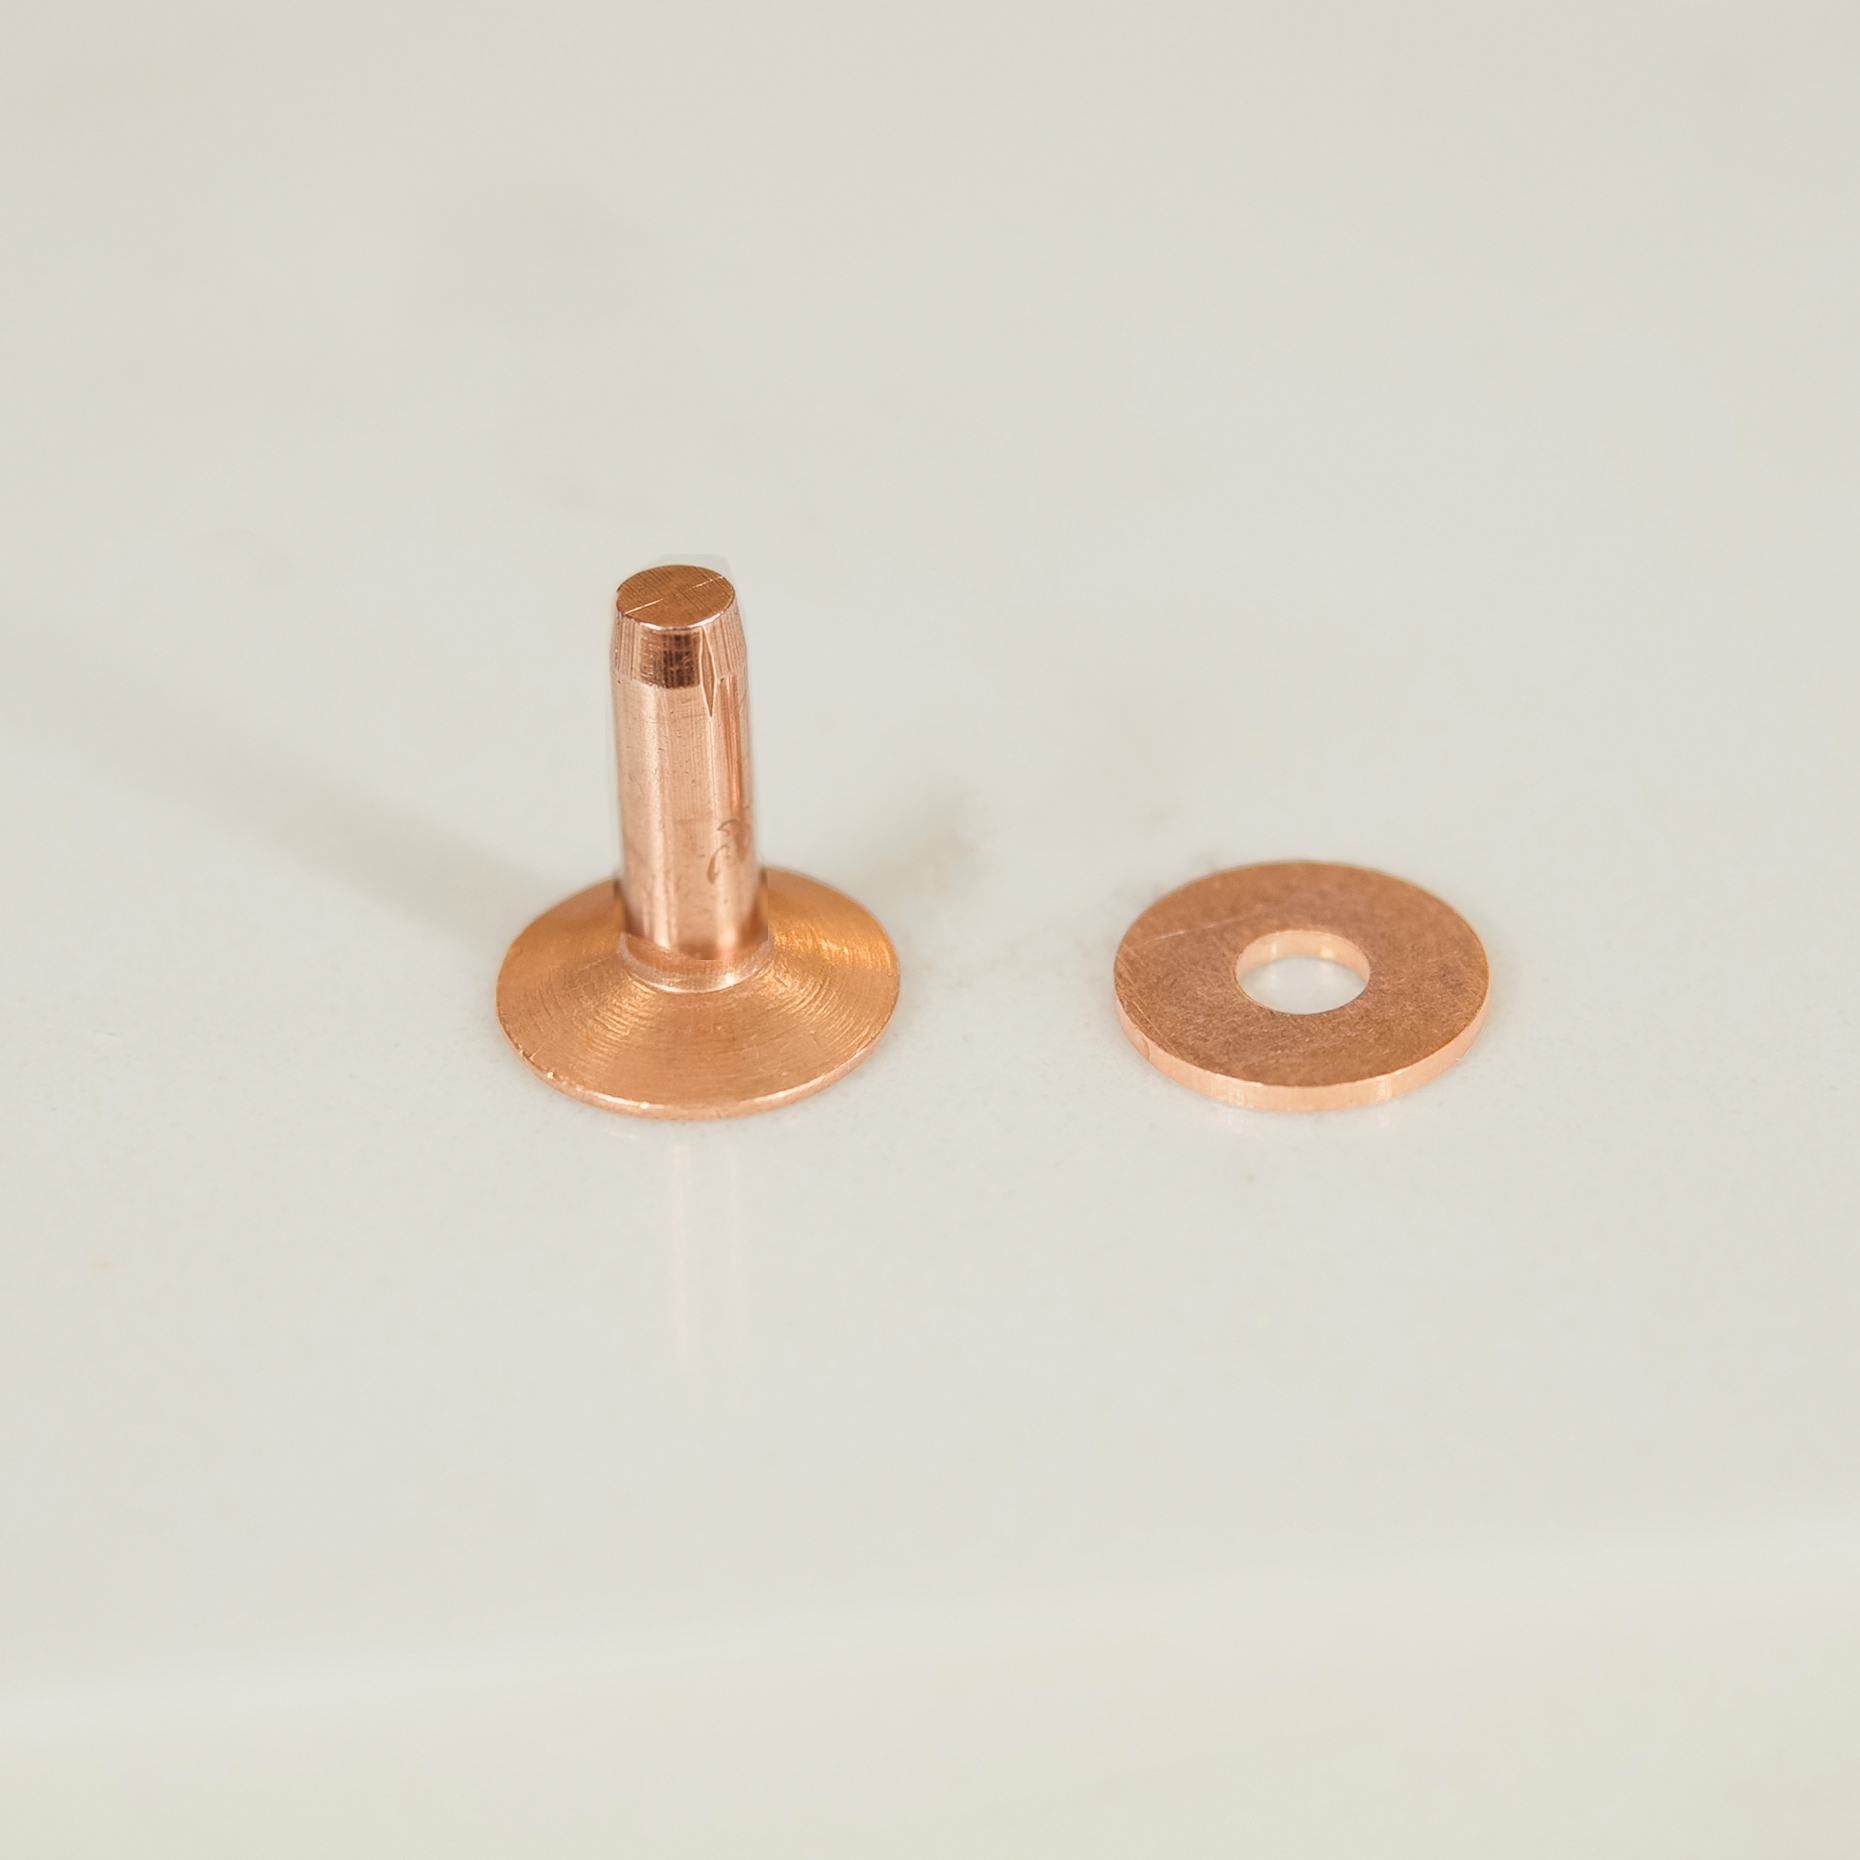
Copper rivets have a typical warm, reddish tone. On leather goods they look bold and handcrafted, and they stand out where you want the rivet to be a visible part of the design.
Brass rivets have a golden tone and go well with brass hardware. If you use brass buckles, D-rings, snap hooks or other brass components on a piece, a brass rivet helps give the whole product a consistent look.
What happens to copper and brass over time
With both copper and brass, expect their look to change with use. Both metals can darken over time, lose their original shine and develop a patina. This is not a defect but a natural property of these metals.
Moisture and water can speed this up. If the piece often comes into contact with water, sweat, rain or damp conditions, the rivets may darken faster or show surface oxidation. With long exposure to moisture and air, copper can develop its typical blue-green patina. Brass tends to turn darker and duller.
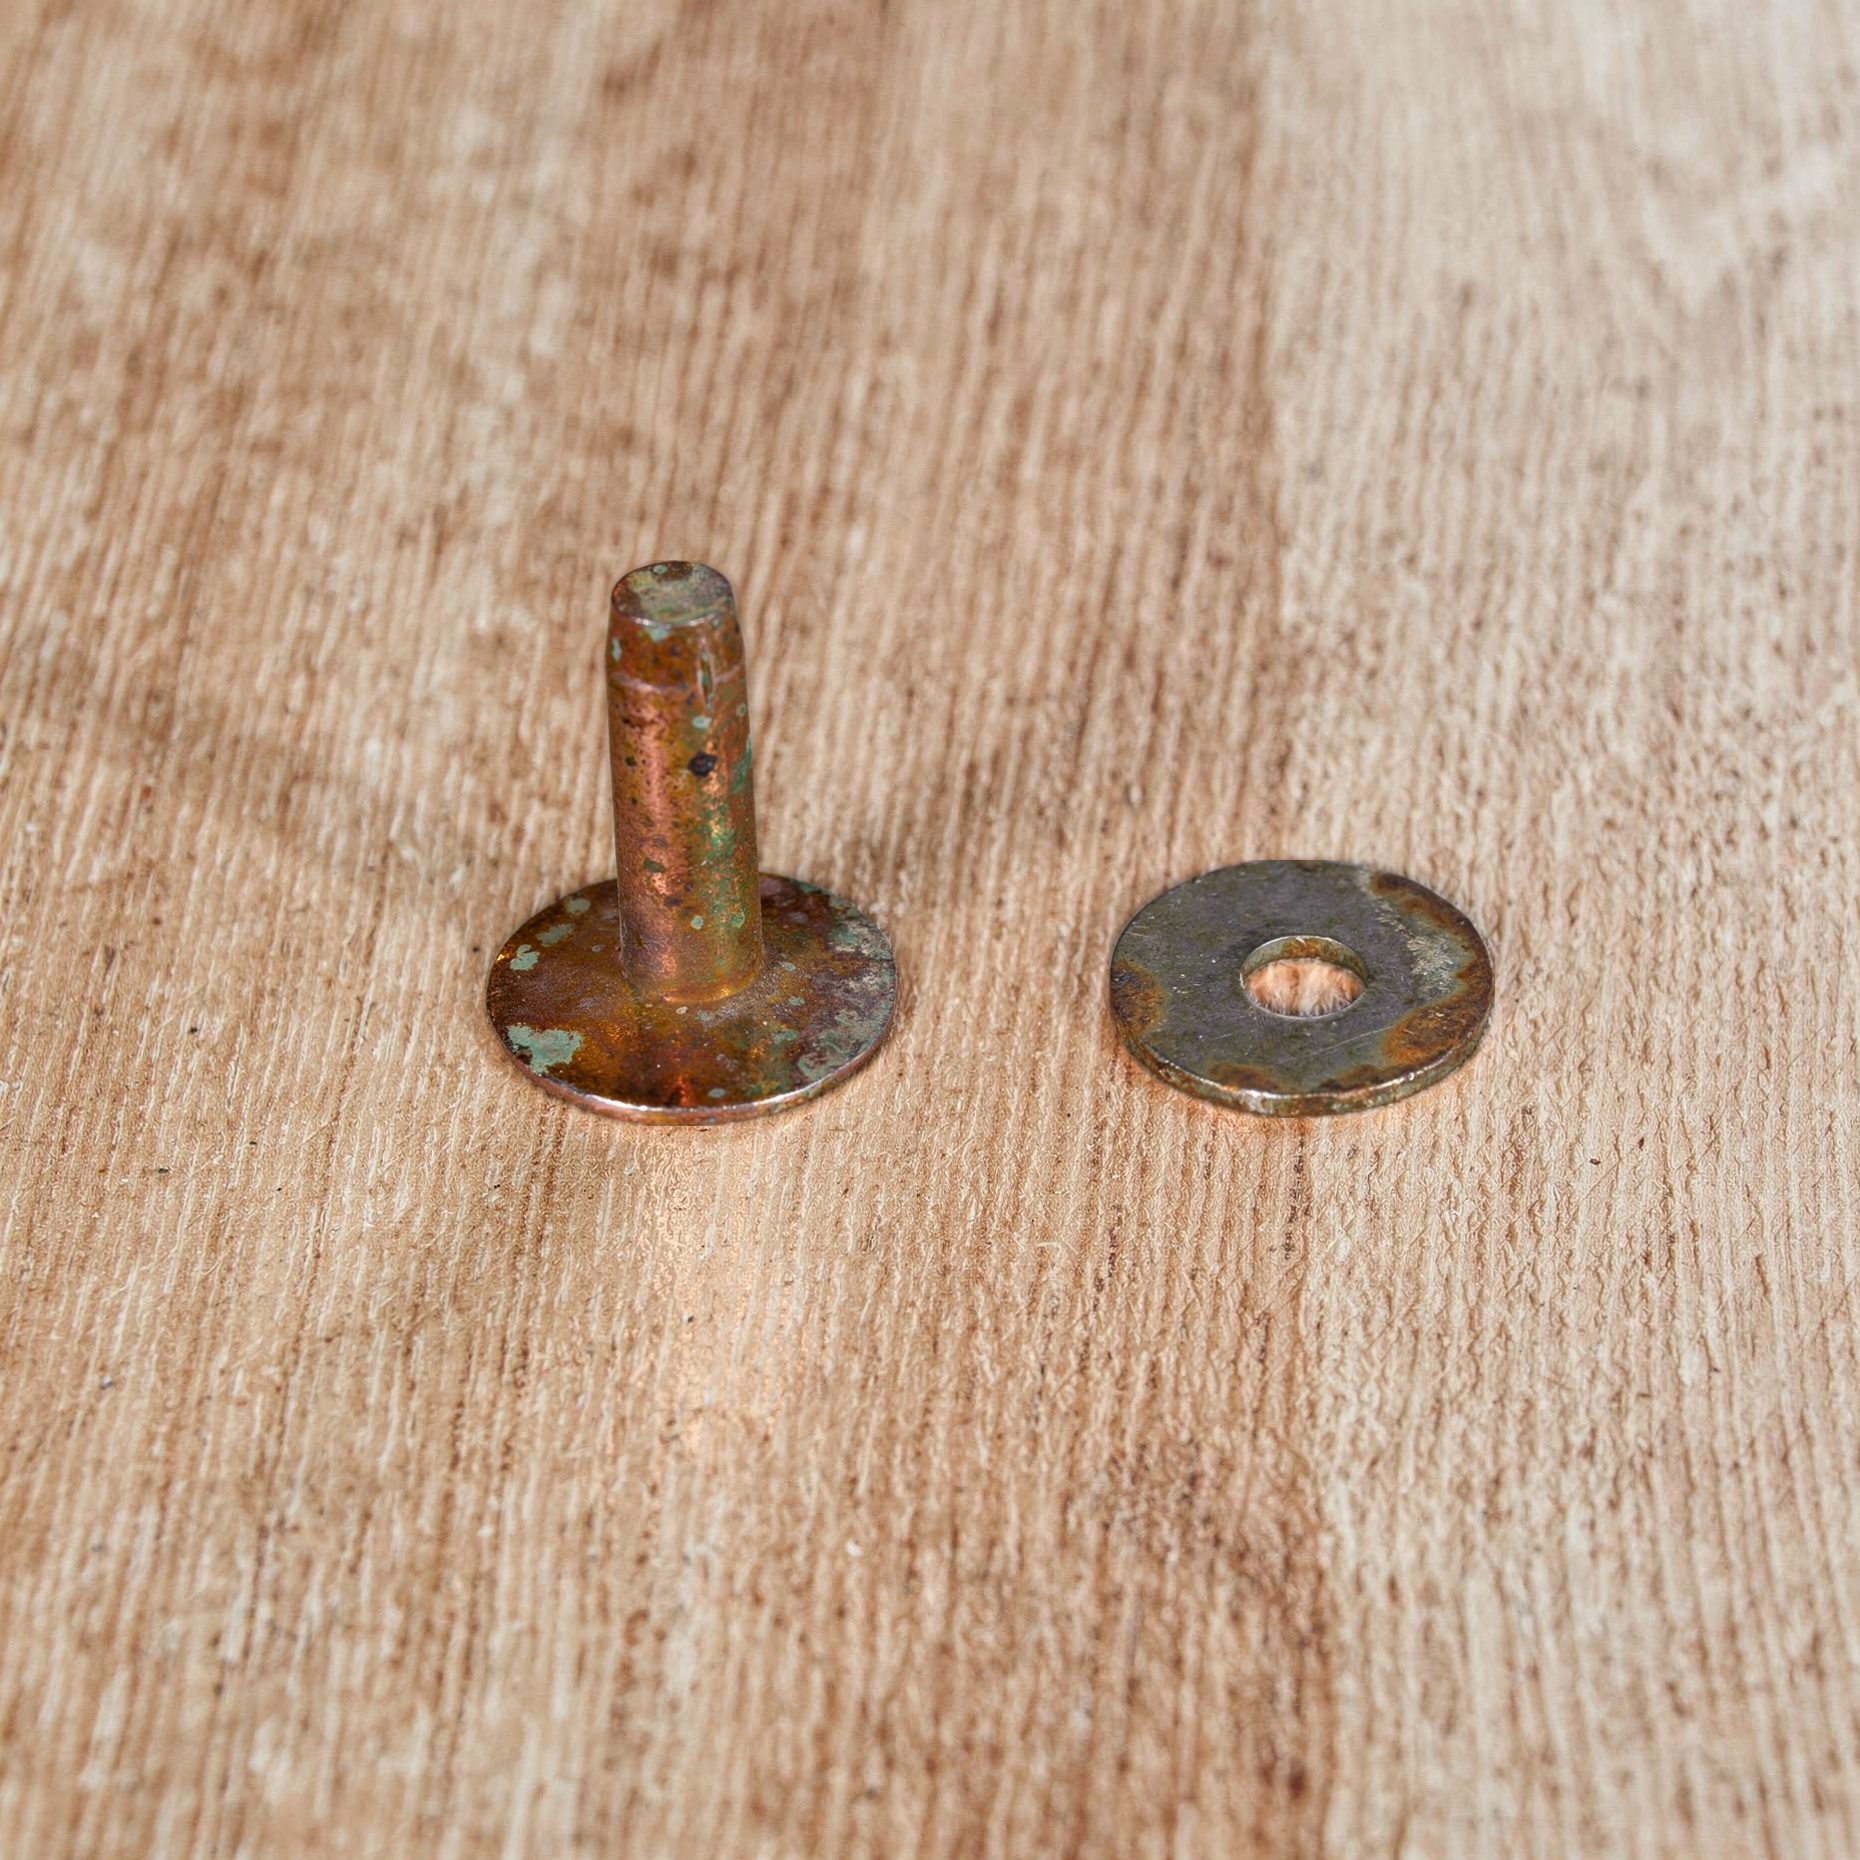
That does not automatically mean the rivet is bad or no longer works. On copper, patina is a normal, natural reaction of the surface, and under some conditions it can even form a protective layer. With brass, keep in mind that it is an alloy of copper and zinc, and long or harsh exposure to water and the environment can lead to brass corrosion. So for products that will often get wet, plan not only for the look but also for checking the joint regularly.
If you want the rivets to stay shiny longer, keep them dry, wipe the piece dry after it gets wet and give the rivets a gentle clean or polish from time to time. If, on the other hand, you don’t mind a natural patina, copper and brass rivets can take on a more pronounced handcrafted look over time.
How to choose the right rivet size
With copper and brass rivets and burrs, you mainly choose the rivet size and the shank length. Product descriptions may also call the shank the post; in this article, we mean the straight part of the rivet that passes through the material and takes the burr.
Rivet size
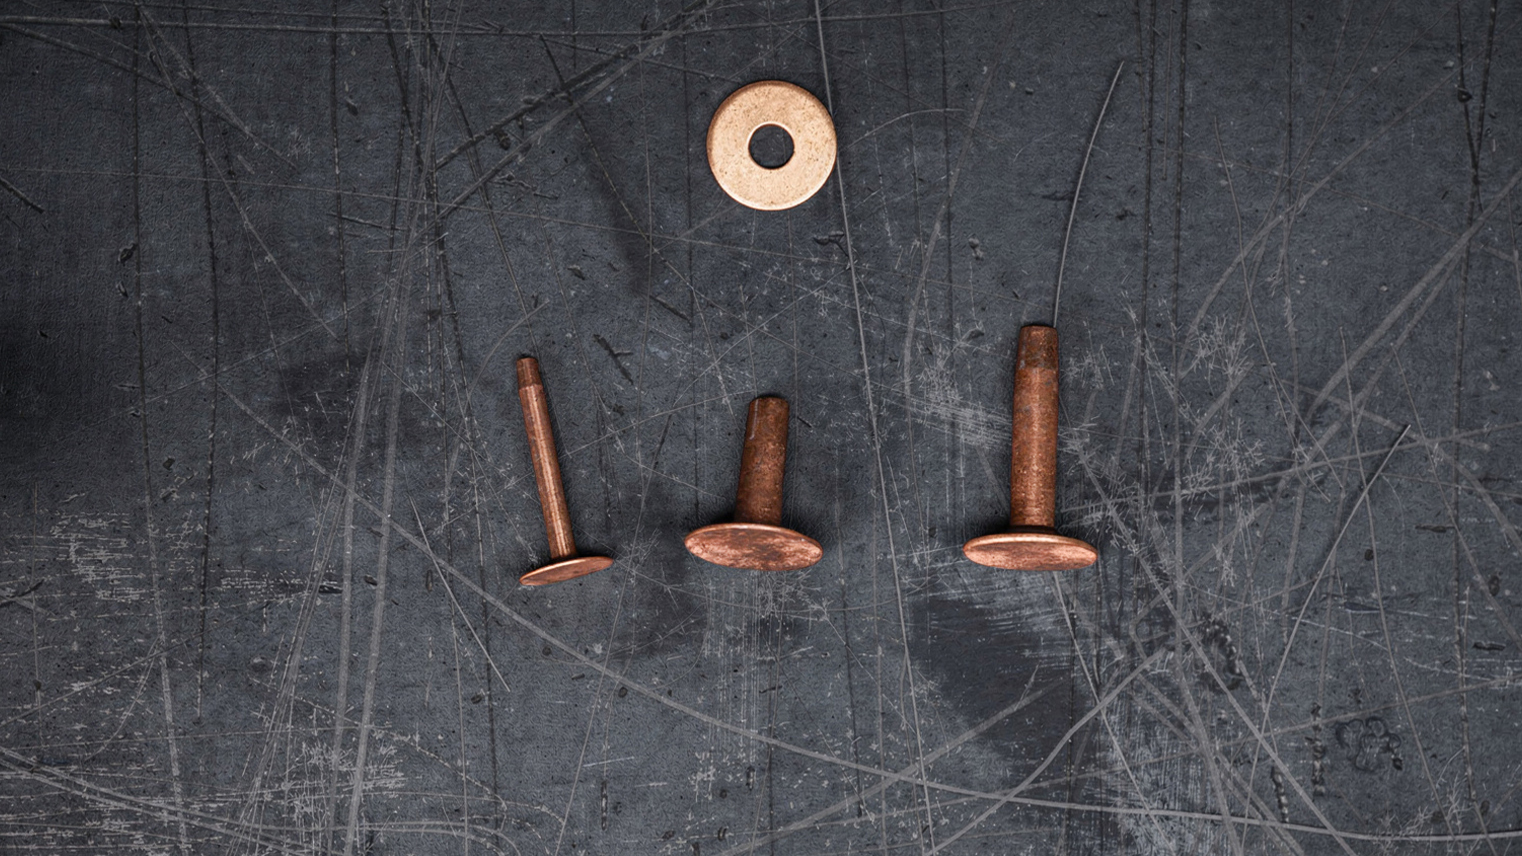
We carry rivets and burrs in two sizes: with a 9 mm head (3 mm shank, 3.3 mm for copper) and with a 12 mm head (4 mm shank). Shank lengths are 14, 20 and 26 mm. The larger rivet has a larger head and a thicker shank; the smaller rivet has a smaller head and a thinner shank.
For smaller items or narrower pieces of material, the smaller rivet is the better fit. For larger items, wider pieces, thicker material or joints under more stress, choose the larger rivet.
Think about the look as well. On the finished piece, you will see the original rivet head on one side and the peened end of the shank on the other, so the rivet size should match the overall look of the product.
Shank length
Choose the shank length by how many layers of material you are joining and how thick they are together. The thicker the material, the longer the shank you need.
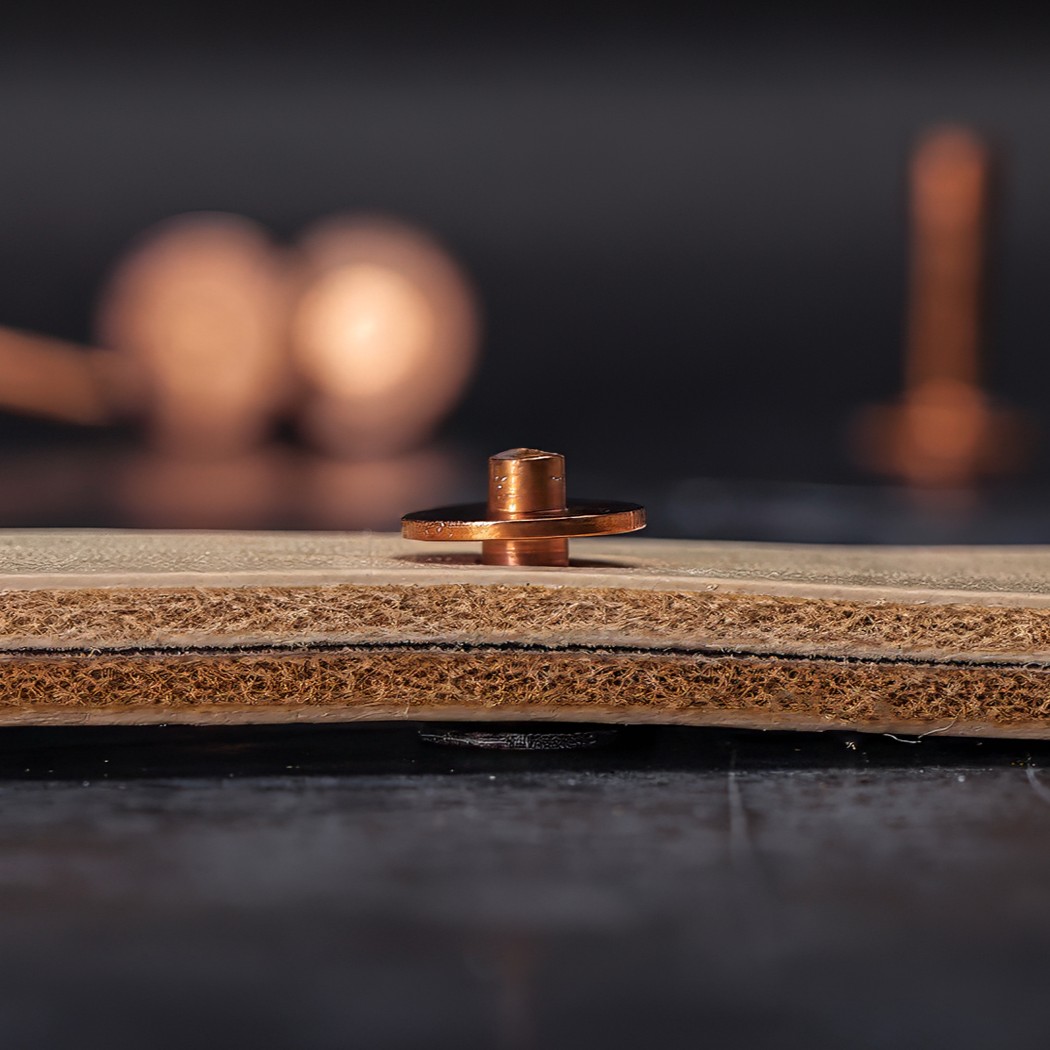
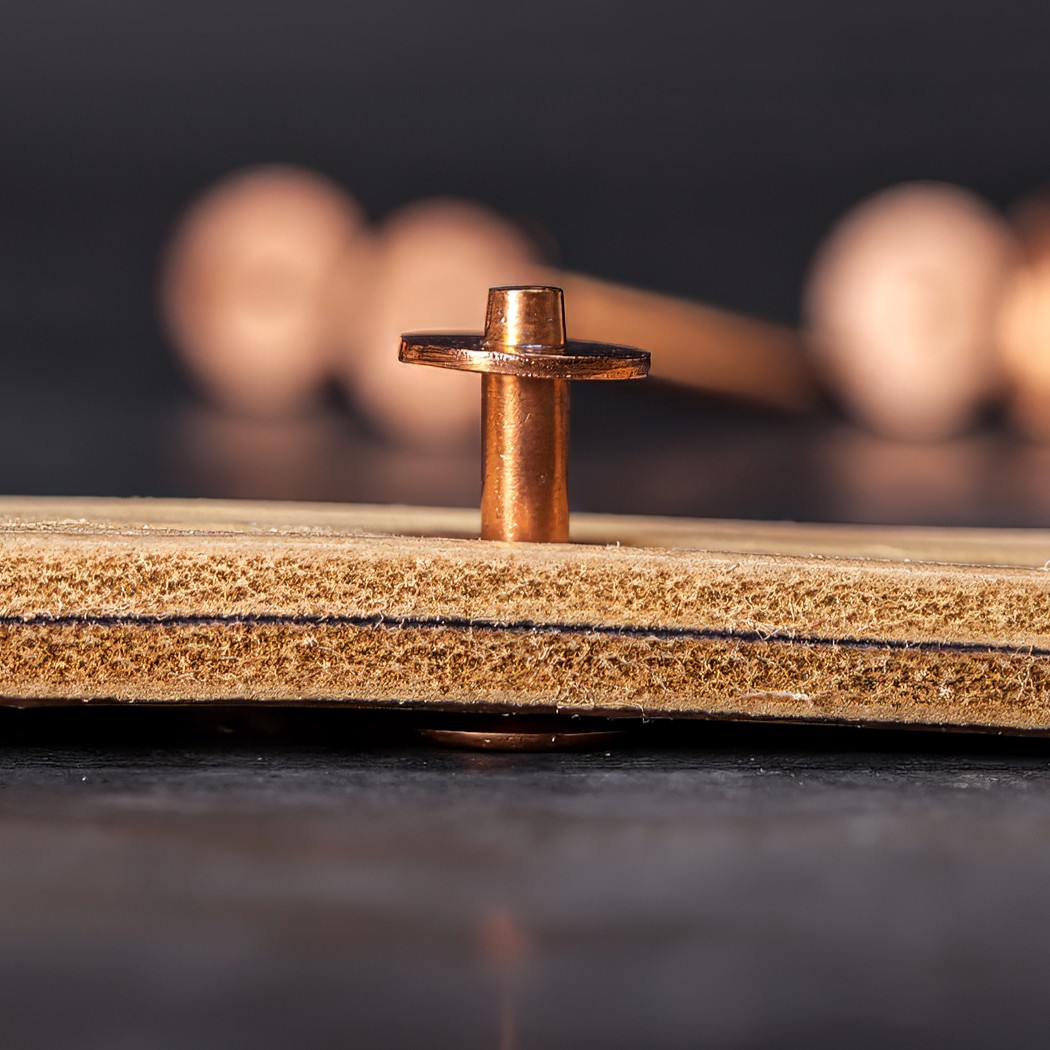
Once the rivet is through the material, there has to be enough room left for the burr and for setting. Pick a shank length that leaves 2 to 4 mm sticking out above the burr once it is seated; that is the metal you will peen into the head. So add the thickness of the burr plus 2 to 4 mm to the thickness of the material.
A shank that is too short cannot be set properly. A shank that is too long is less of a problem, but you will have to trim it correctly after seating the burr.
How to prepare the hole
Punch the hole to match the shank diameter: a 3 mm punch for a 3 mm shank and a 4 mm punch for a 4 mm shank (3 mm also works for the copper rivet with a 3.3 mm shank). Always test the size on a scrap of the same material. The rivet should go through, but it should not wobble around in the hole.
If the hole is too small, you will not get the shank through, or you will damage the material. If it is too big, the rivet will not sit well and the joint may not hold properly.
Tools you will need
Before you start riveting, get the rivet, the burr and the right tools ready:
- copper or brass rivets and burrs,
- a hole punch or rotary punch pliers for the hole,
- a rivet setter to match the rivet head diameter,
- a hammer,
- end-cutting pliers to trim the shank,
- a solid work surface, such as a granite slab or an anvil,
- optionally sandpaper or a small rotary tool to smooth out rough spots in the setter.
The most important tool is the rivet setter. It has two working parts: a hole for seating the burr and a cupped recess for forming the head. With it, you drive the burr down against the material properly and then give the rivet a cleaner finish.
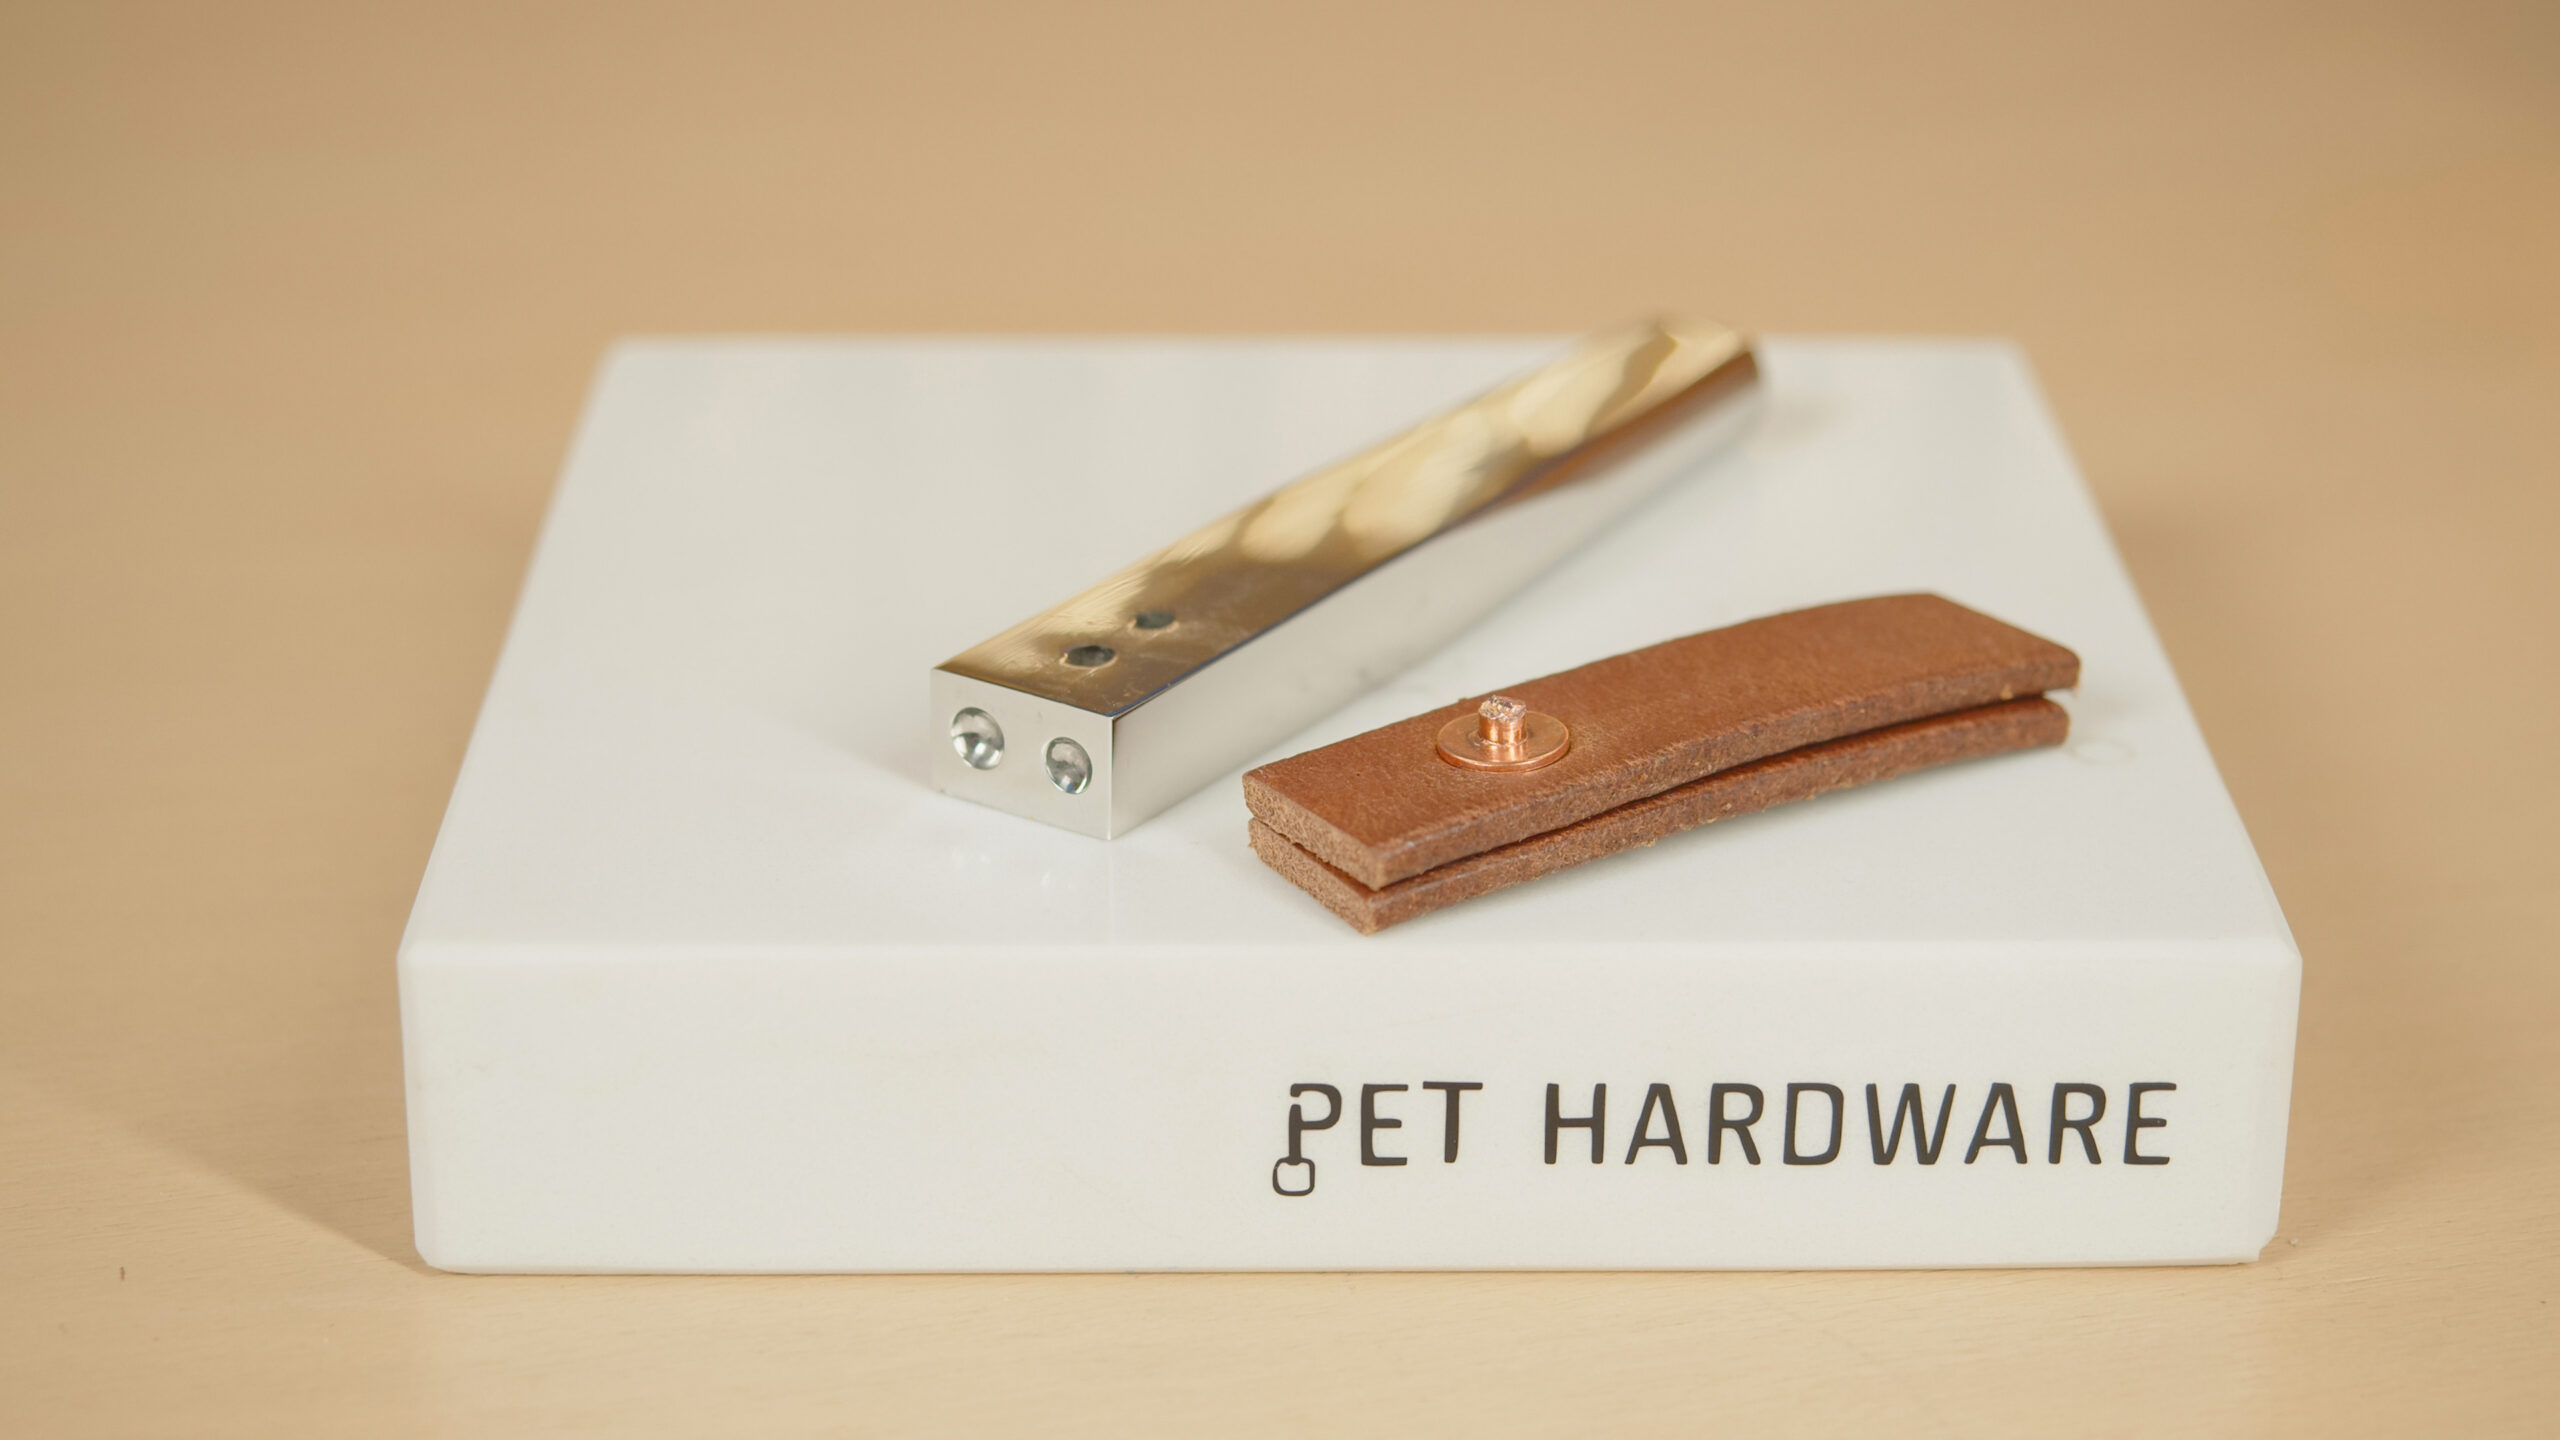
Check whether the recess of the setter has any small burrs or sharp edges left over from manufacturing. If it does, smooth them gently with sandpaper or a small rotary tool so they do not mark the rivet head while you work.
Which side of the rivet should face out
Before you start riveting, decide which side of the piece will be more visible and which side will rest against skin, fur or another sensitive material.
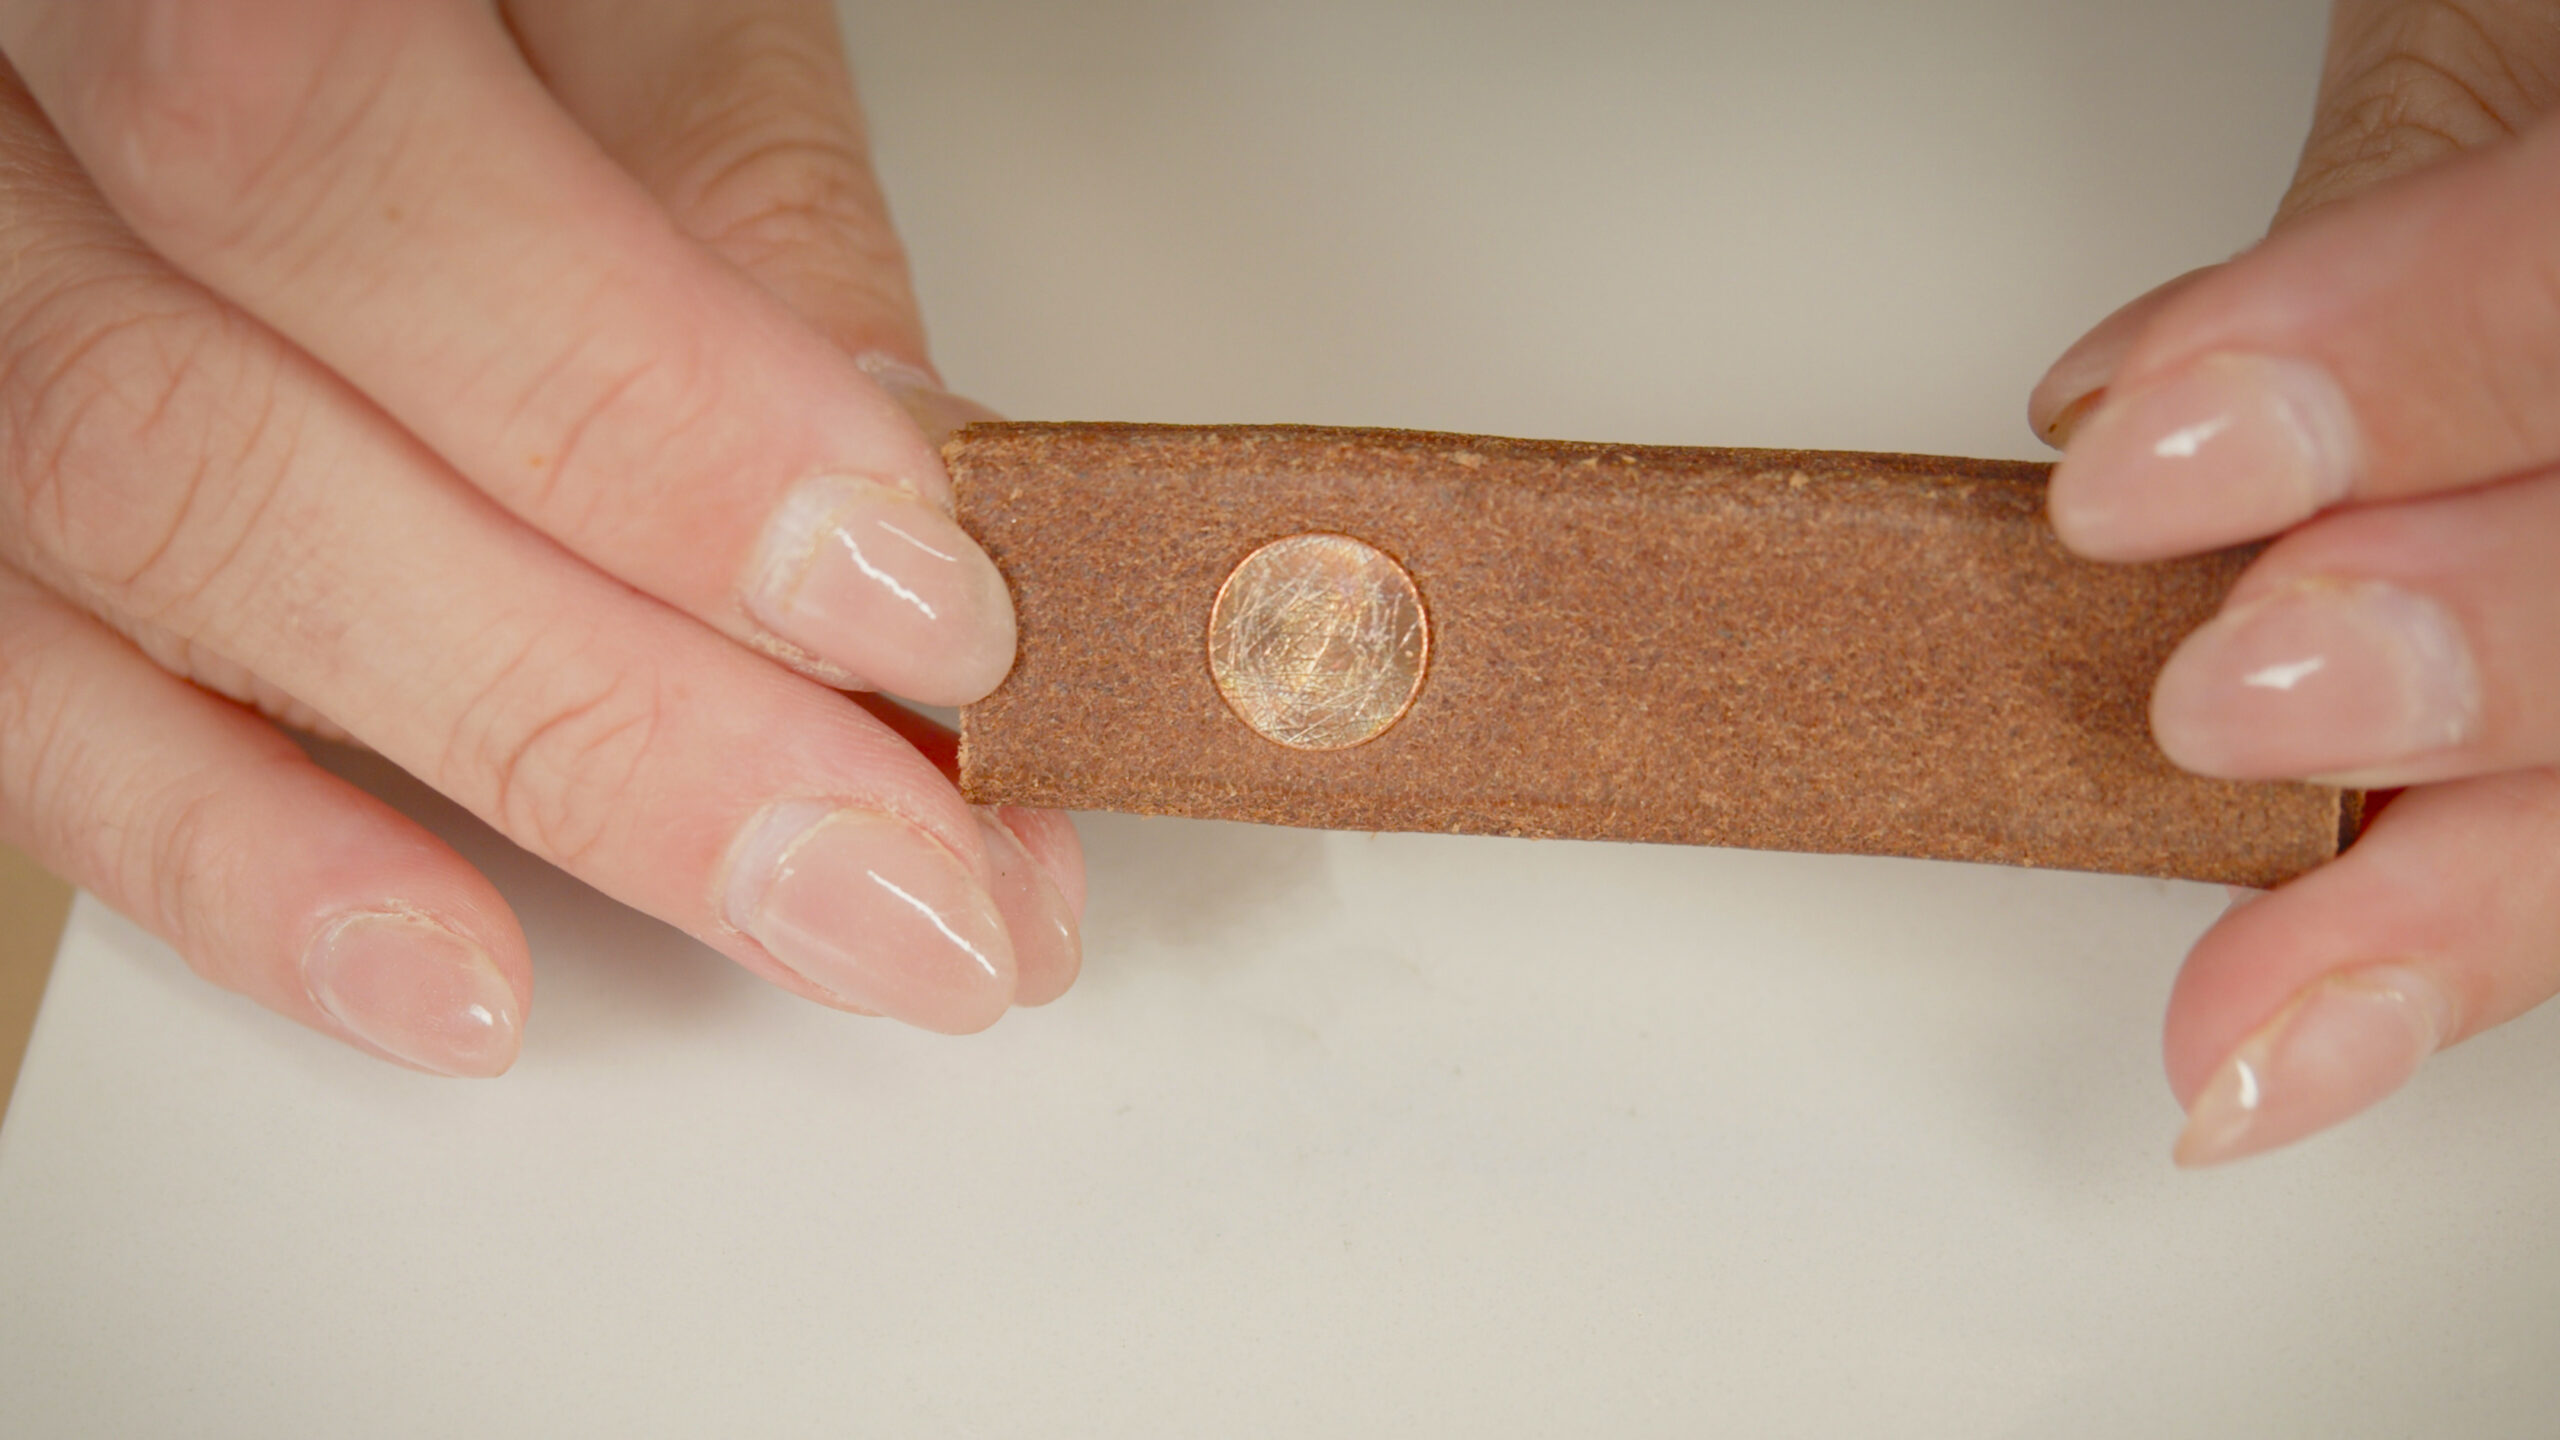
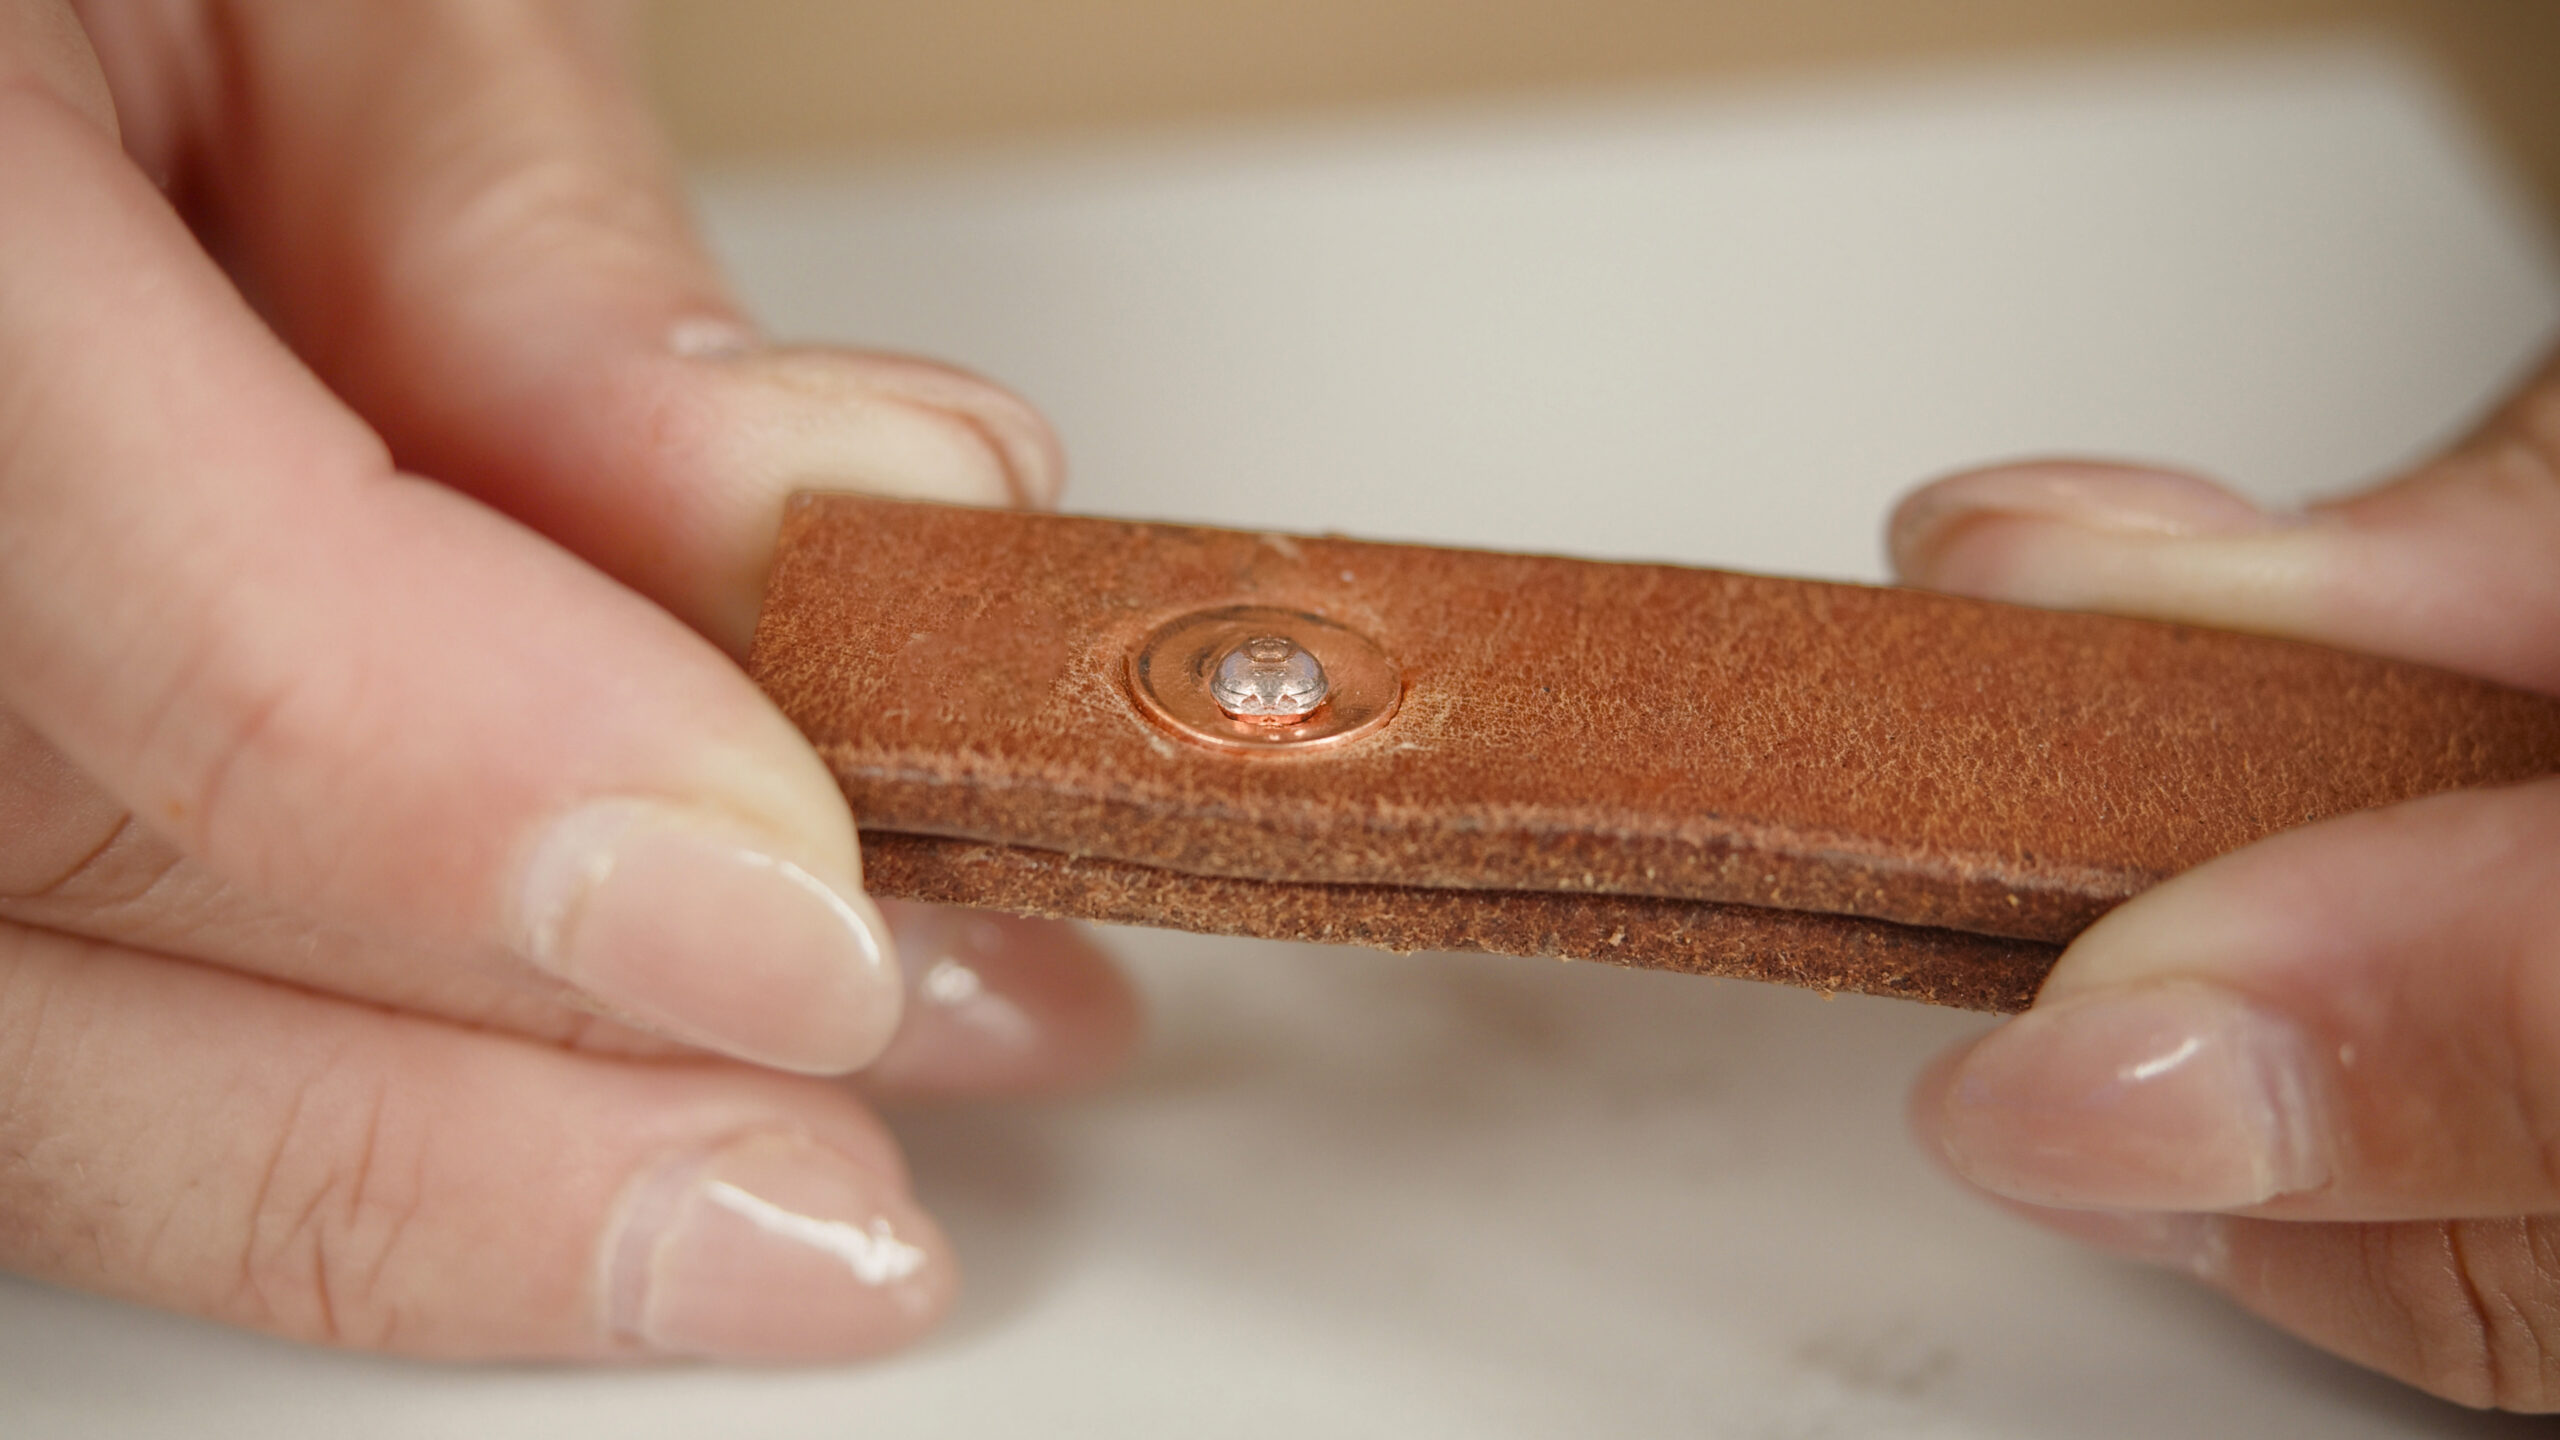
On one side you see the original smooth rivet head; on the other, setting creates a new peened head. Either side can face out, depending on the look of the piece and how you finish the rivet.
If one side of the piece will rest directly against skin or fur, it is safer to turn the original smooth rivet head that way. Always check the peened side carefully to make sure no sharp edge is left on it.
How to set copper rivets step by step
Once you have the right rivet, the hole and the tools ready, you can get started.
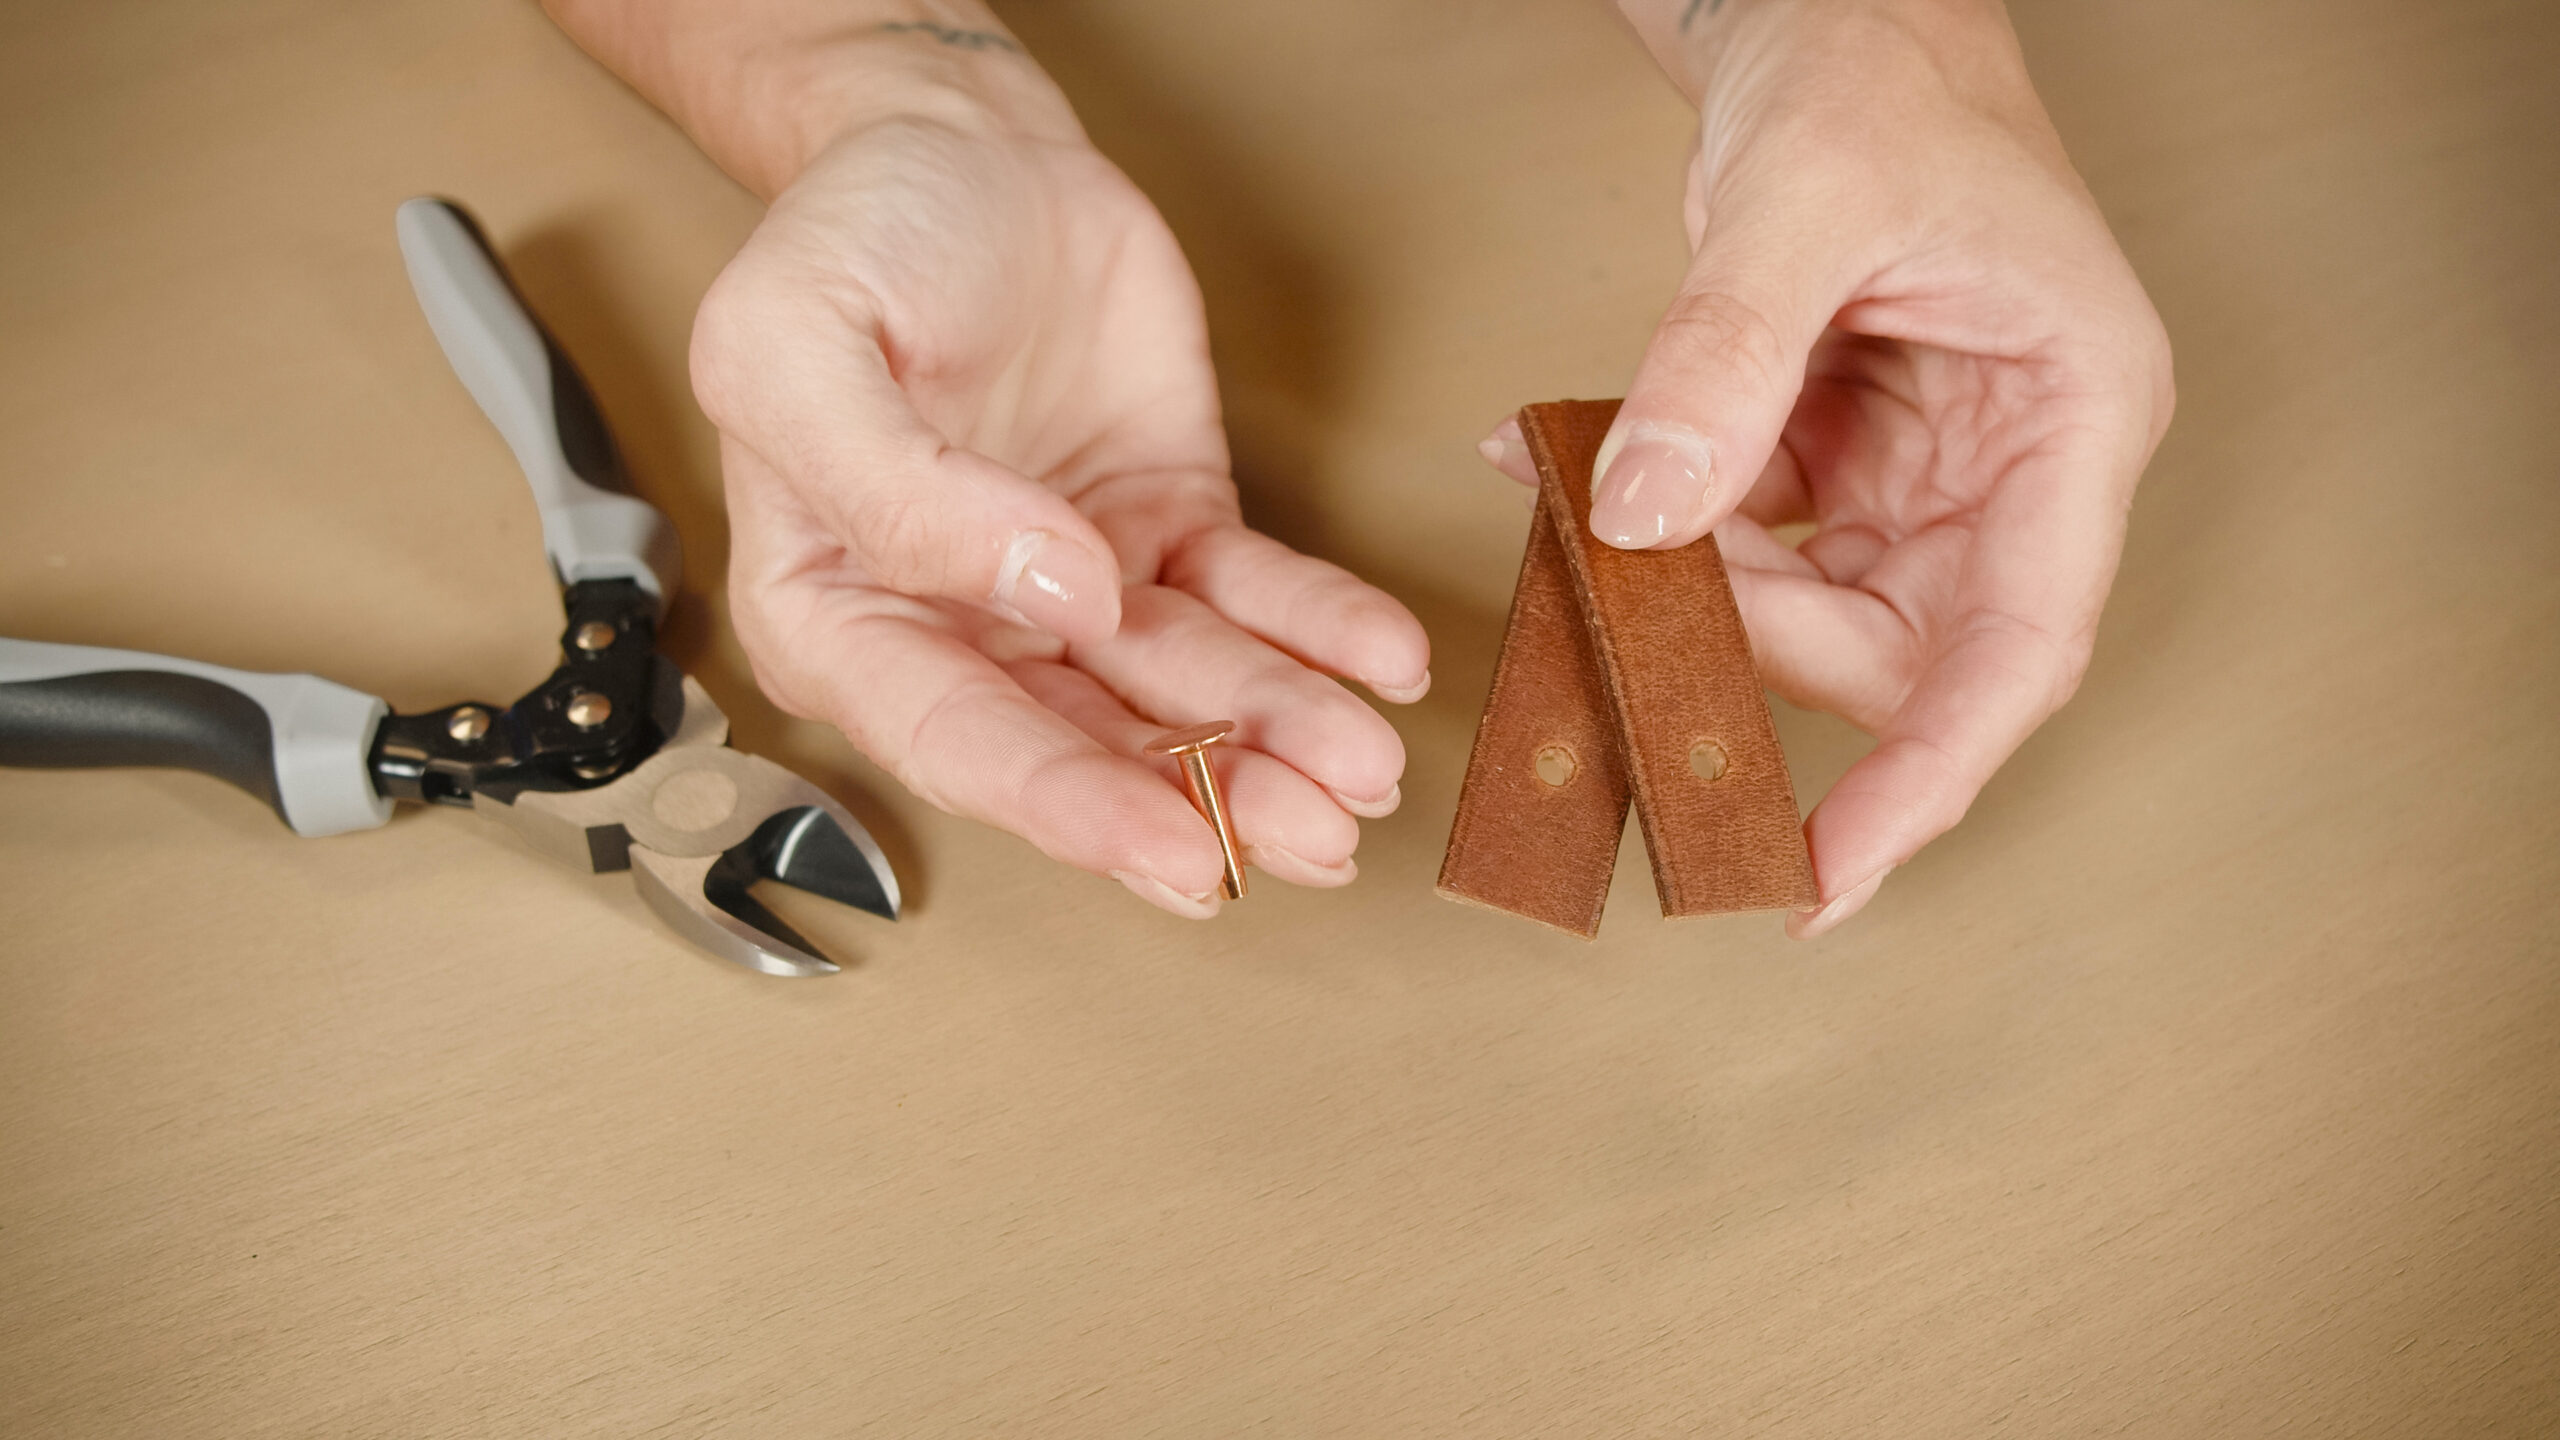
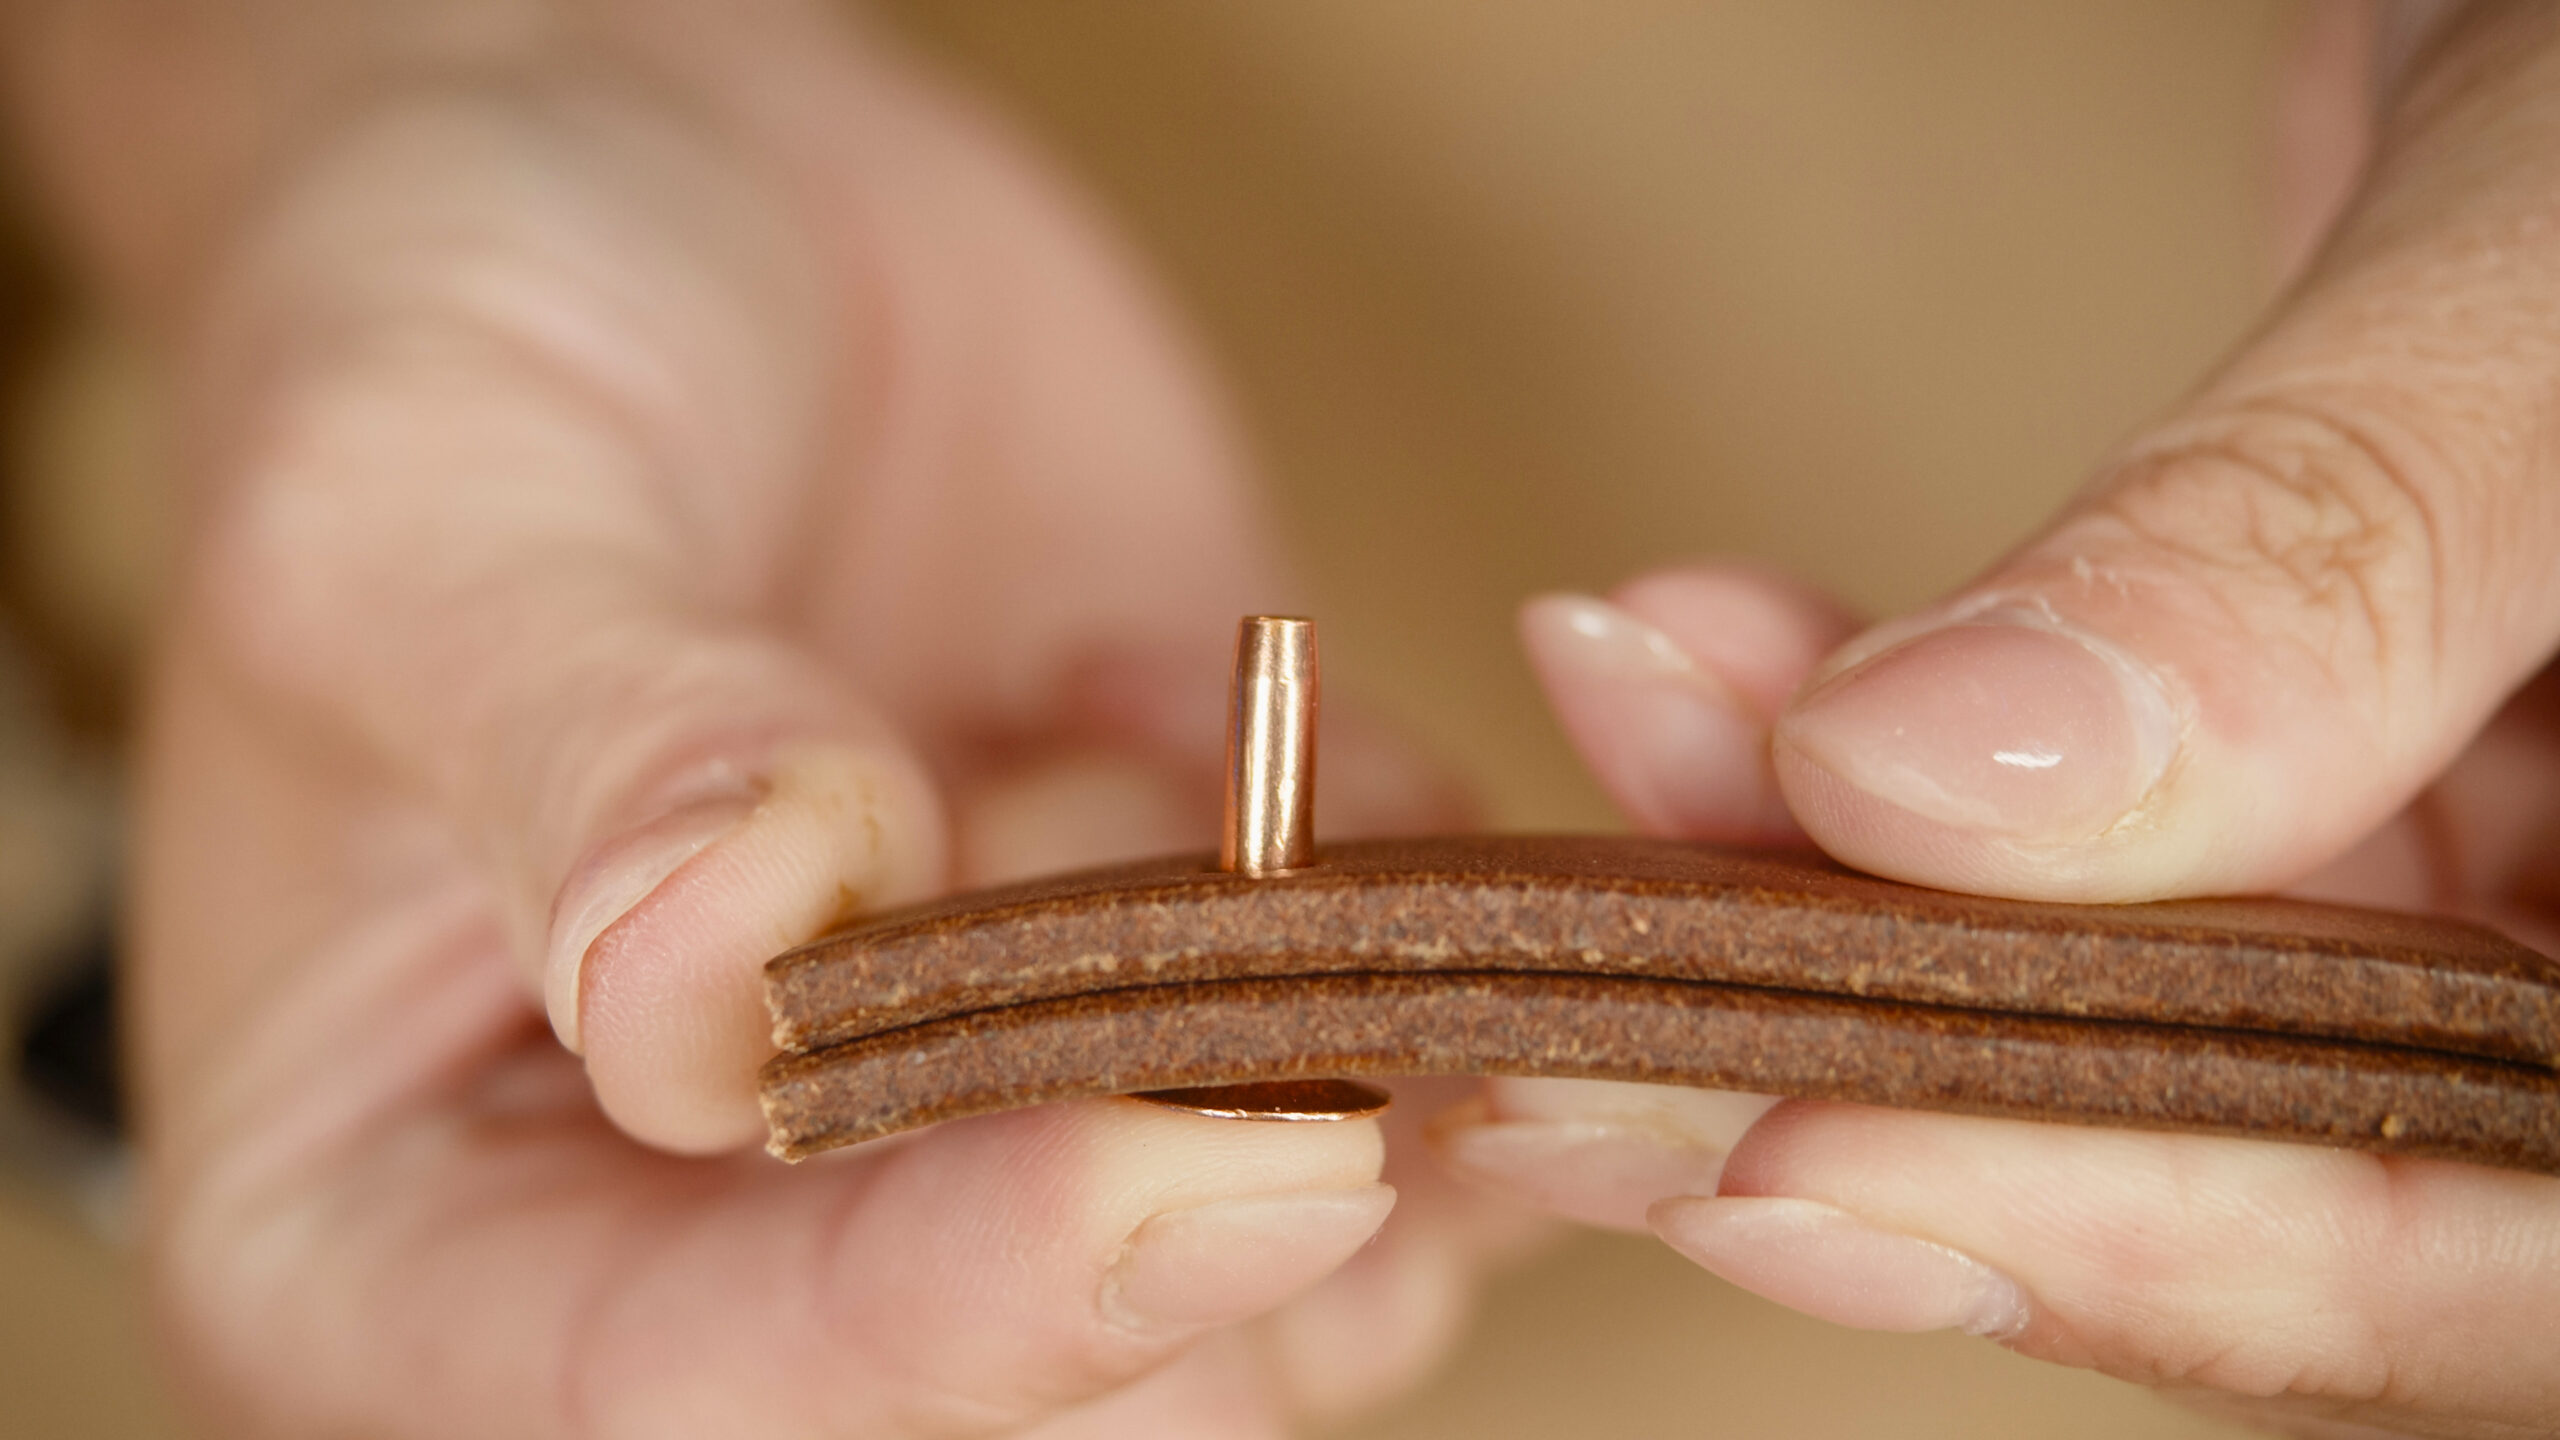
1. Insert the rivet into the hole
Push the rivet through the prepared hole in the material. Decide beforehand which side gets the original smooth rivet head and on which side you will form the new peened head.
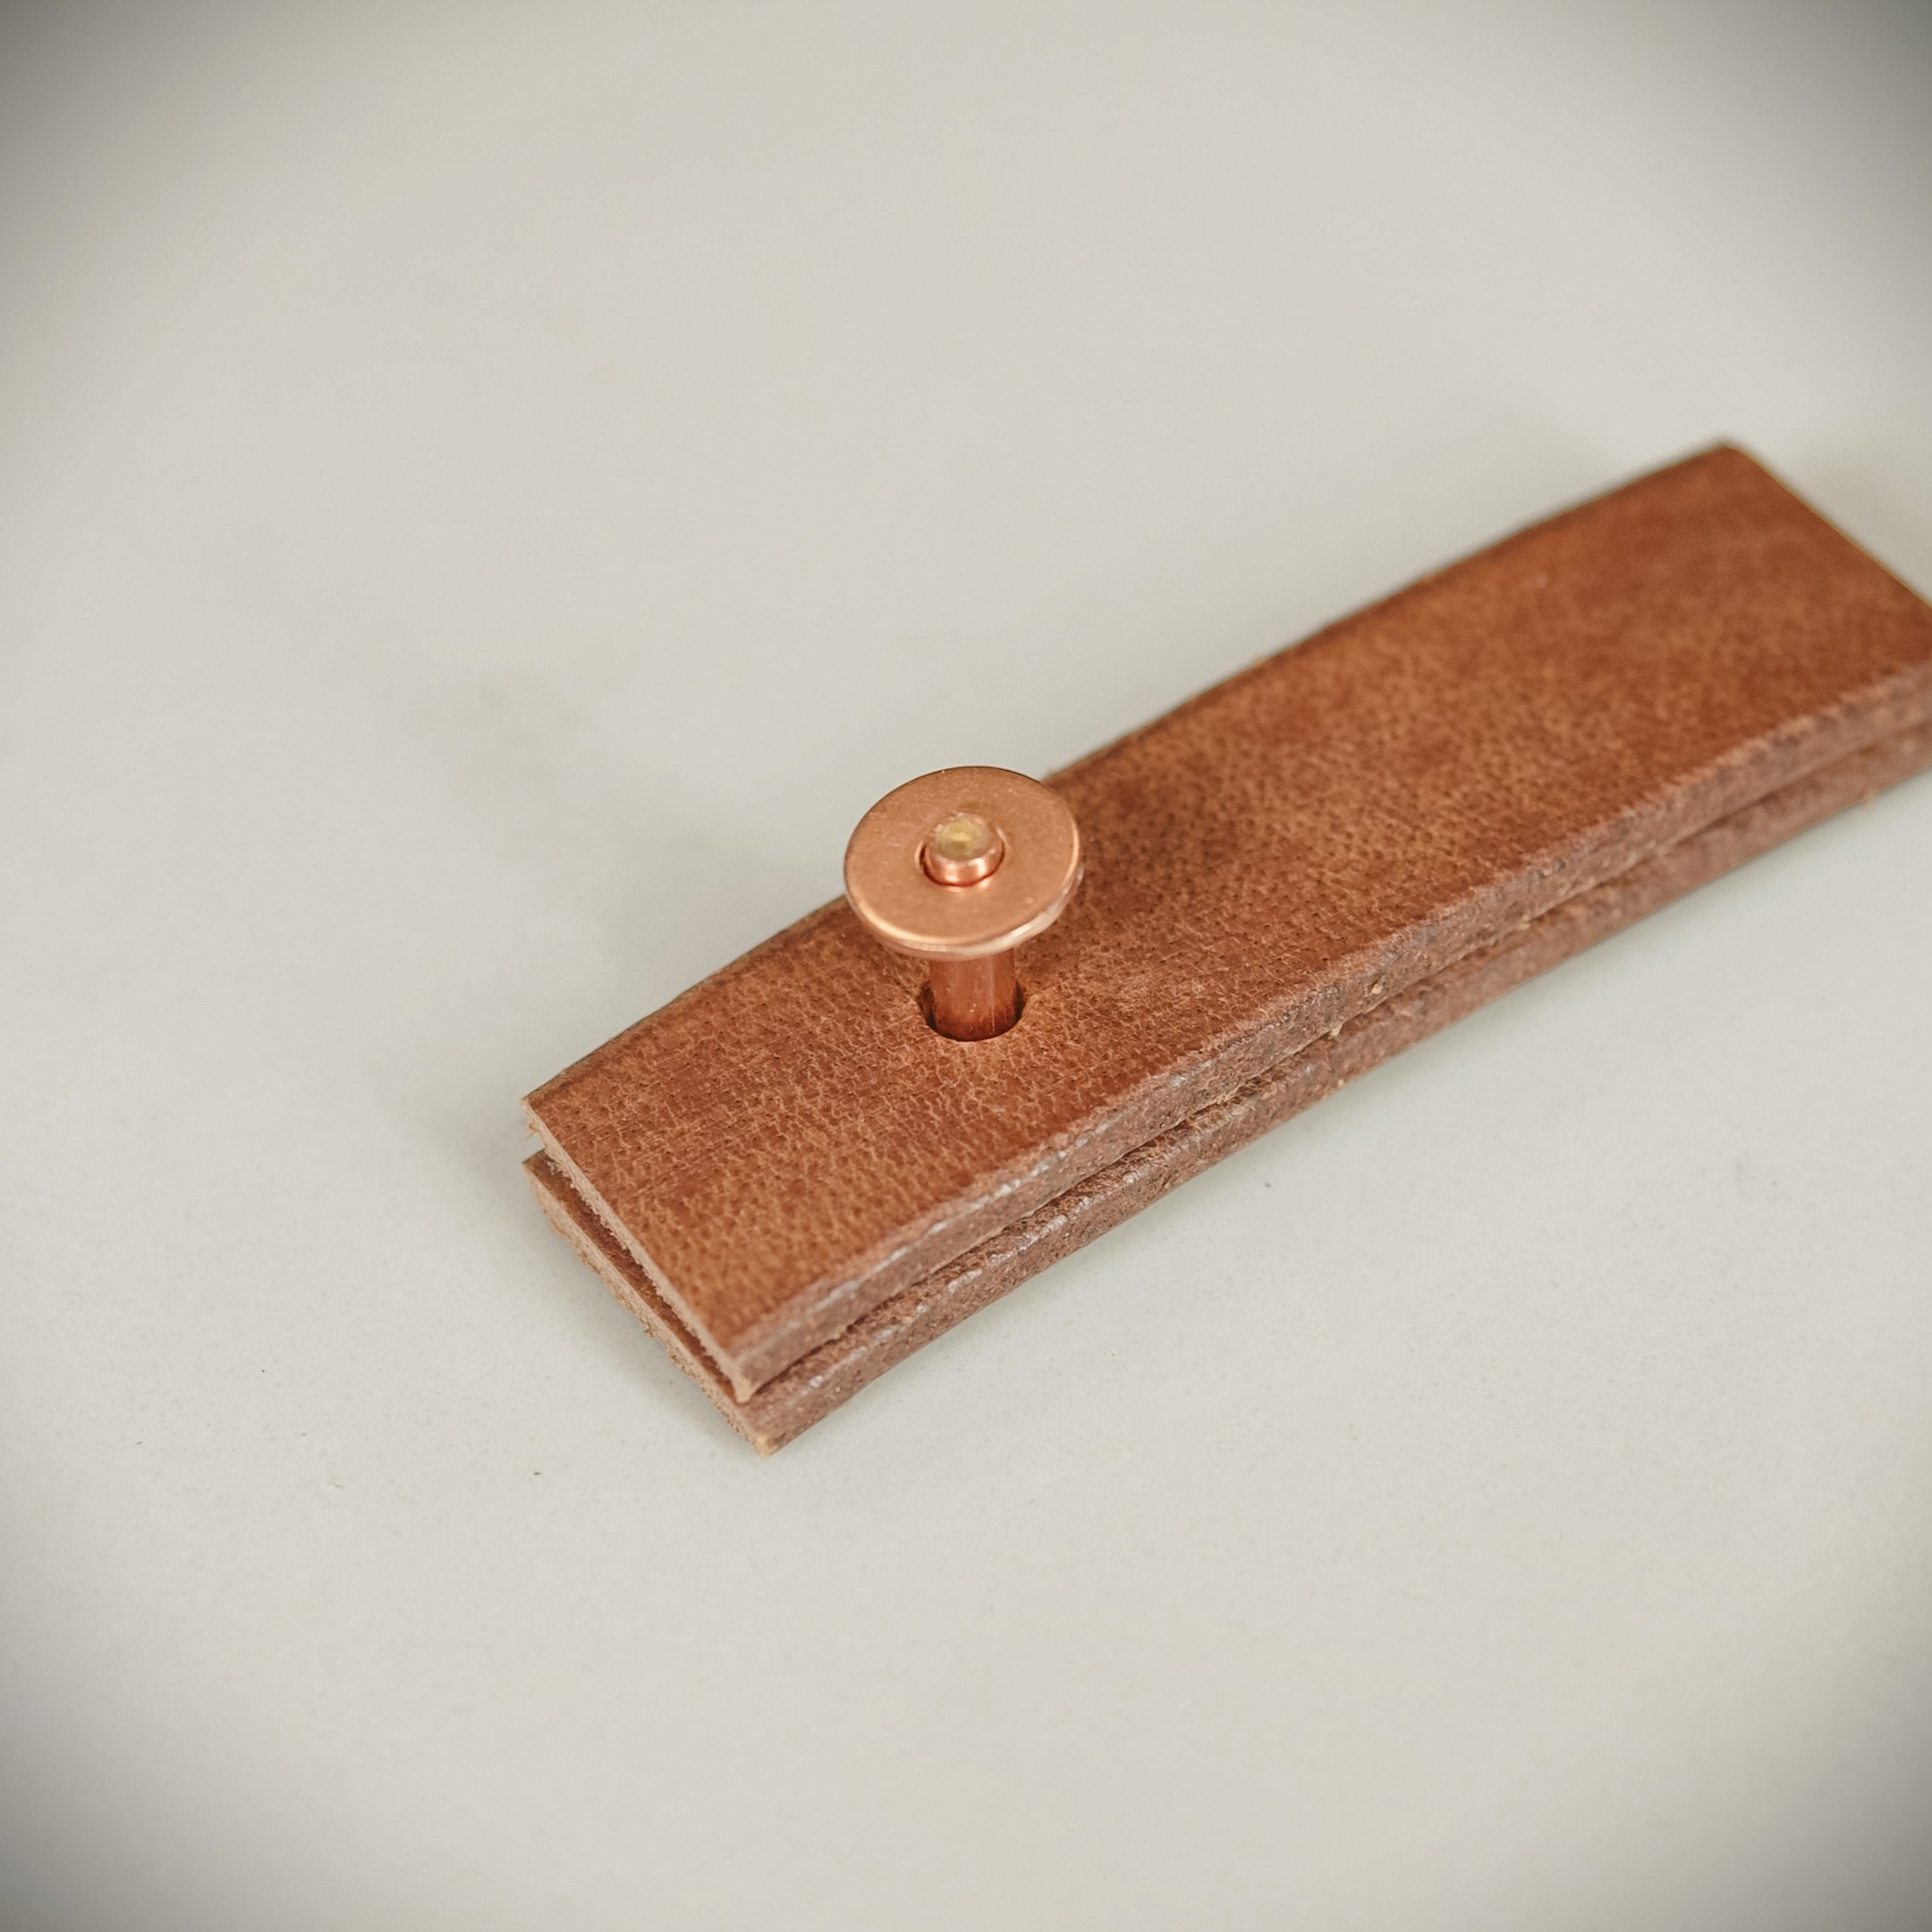
2. Fit the burr
Slip the burr over the shank. The burr goes on the side of the material where you will later trim the shank and form the peened head.
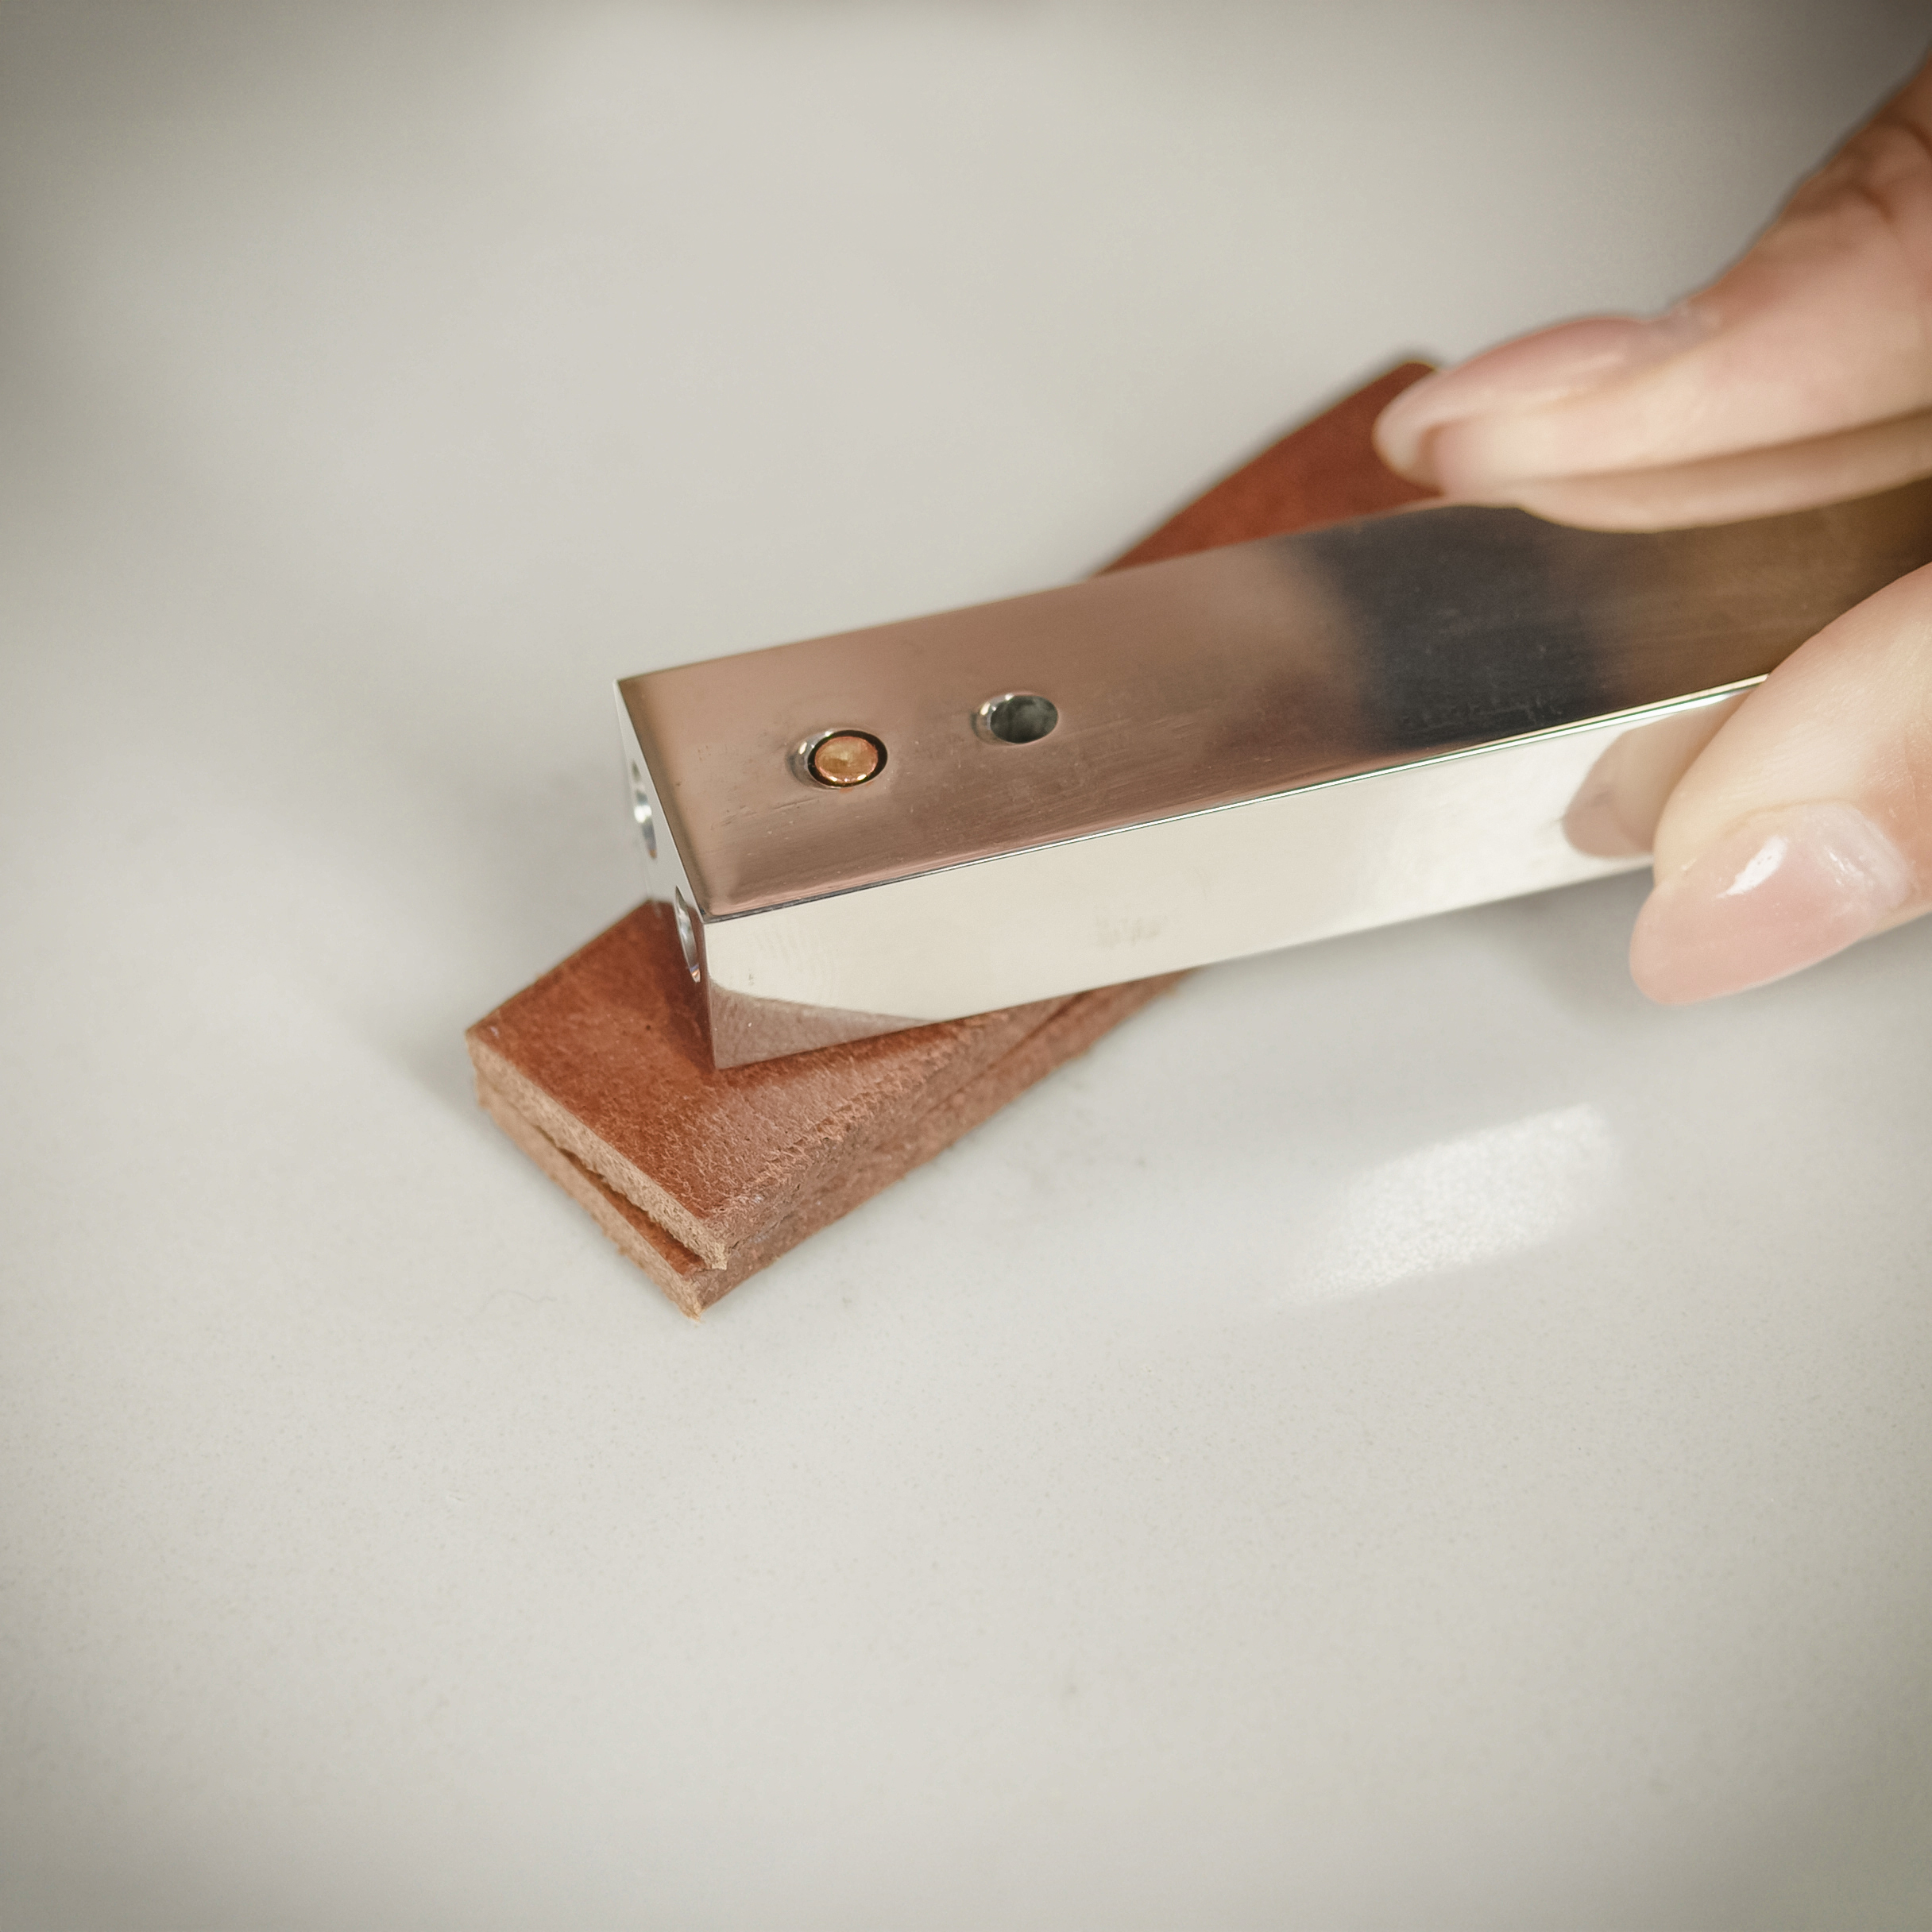
3. Drive the burr down to the material
Place the setter on the shank with the part meant for seating the burr. Don’t drive the burr down with one hard blow. It is better to work gradually with several lighter taps.
The goal is for the burr to sit flat against the material. It should not stay loose, but you also don’t want to drive it too deep into the leather.
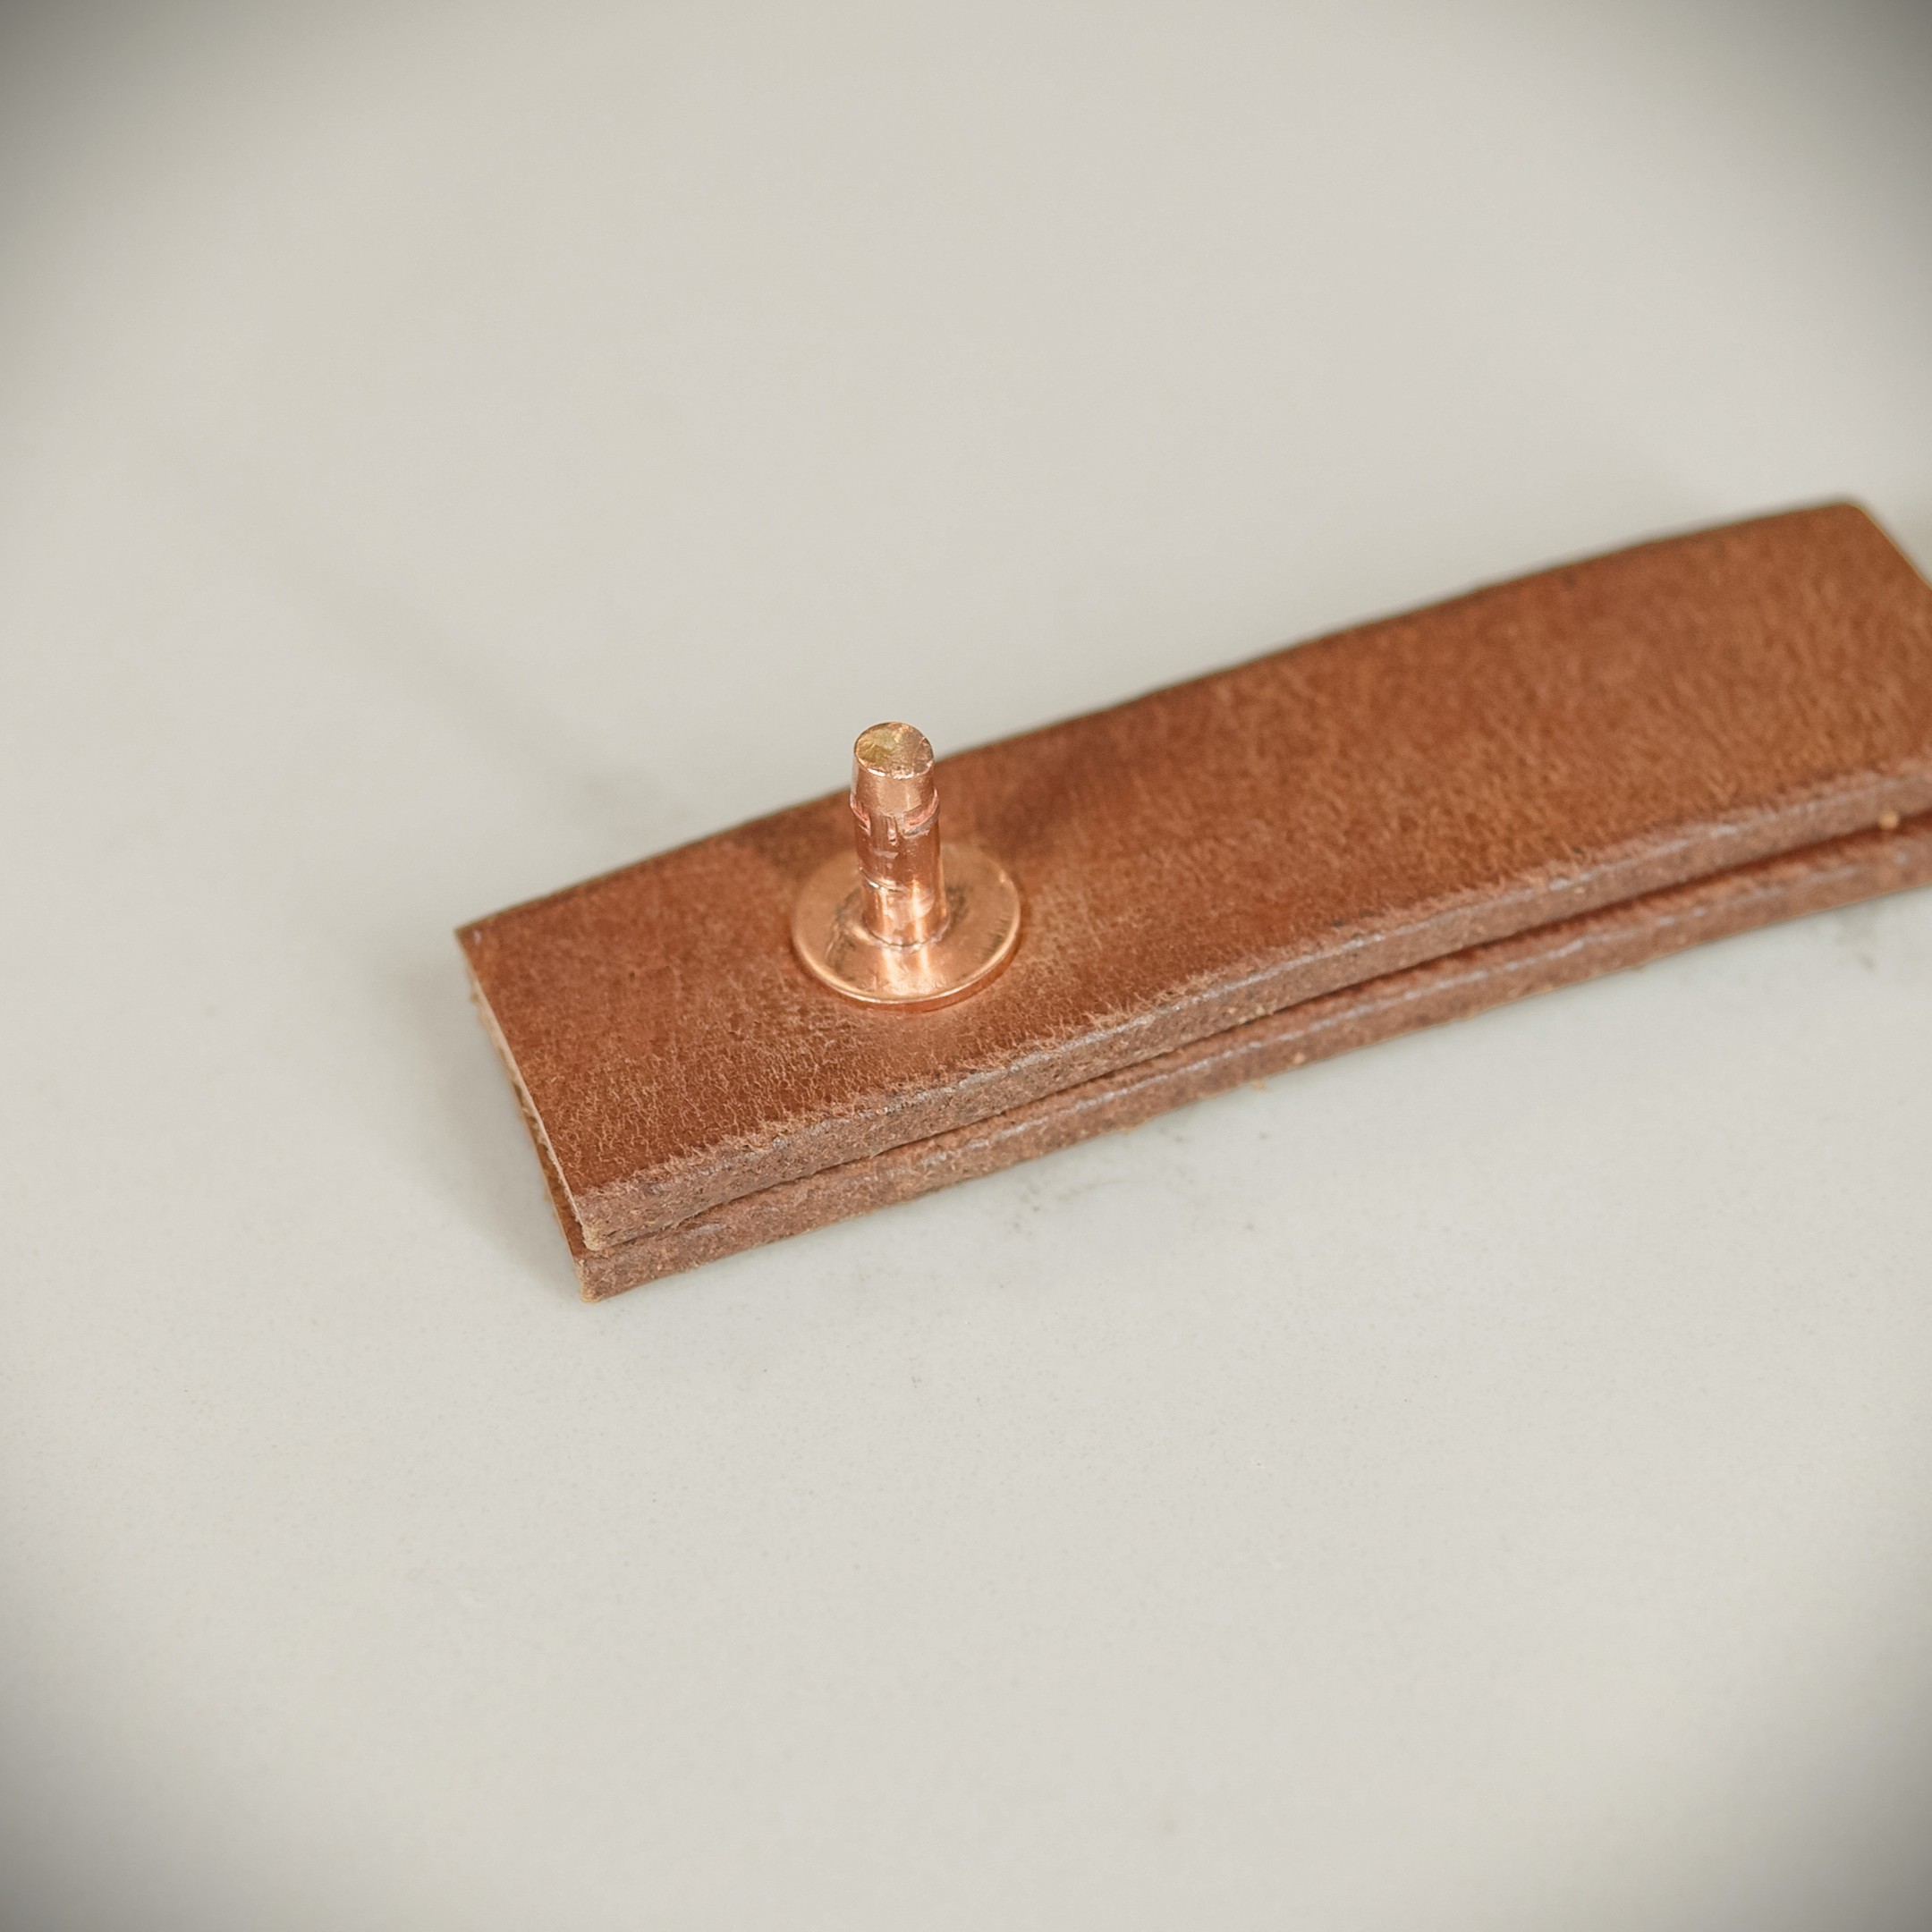
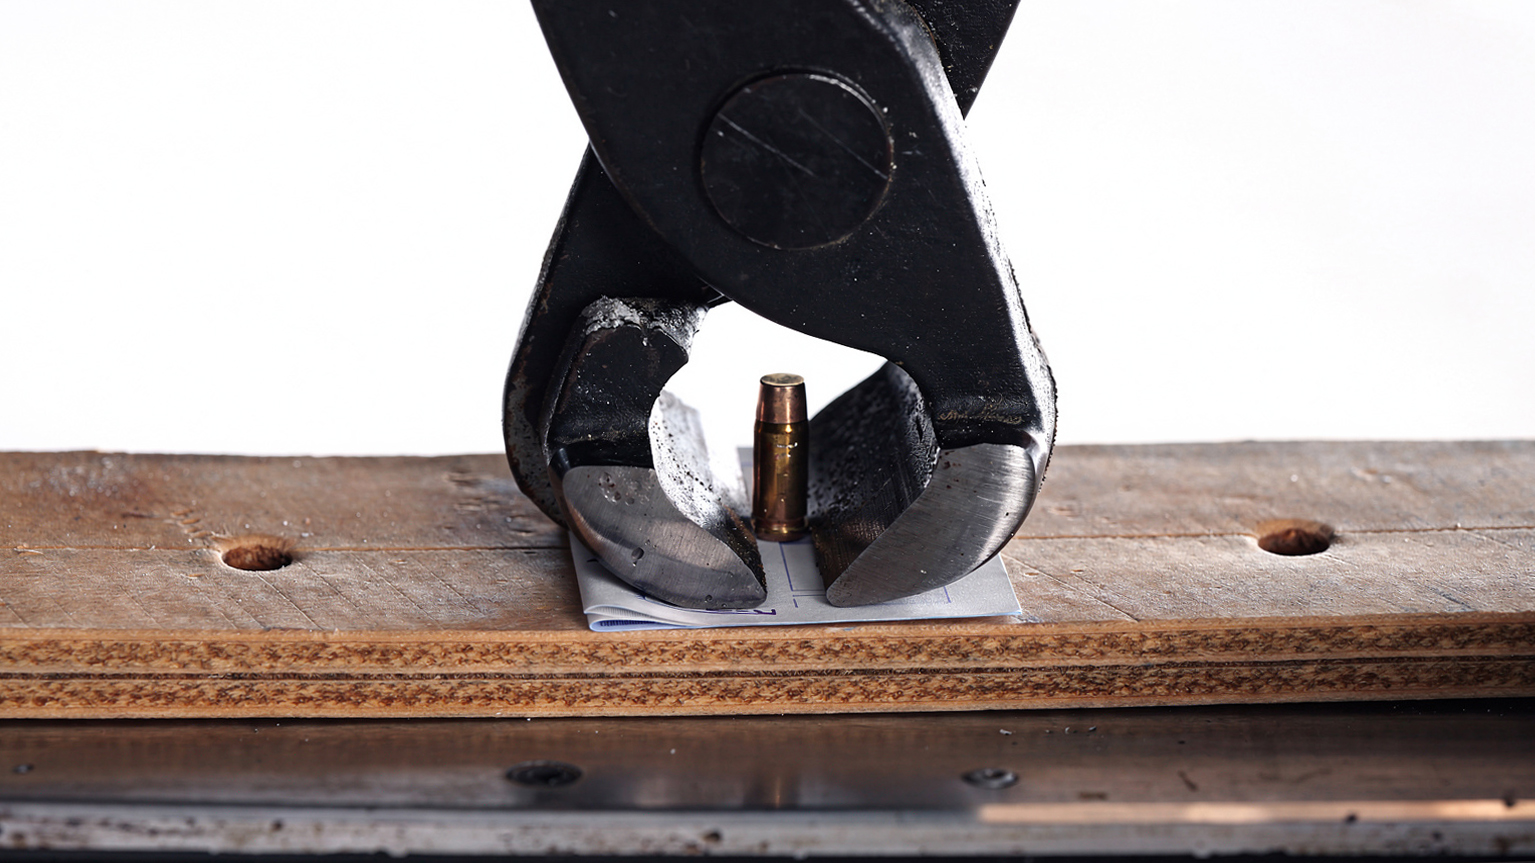
4. Trim the excess shank
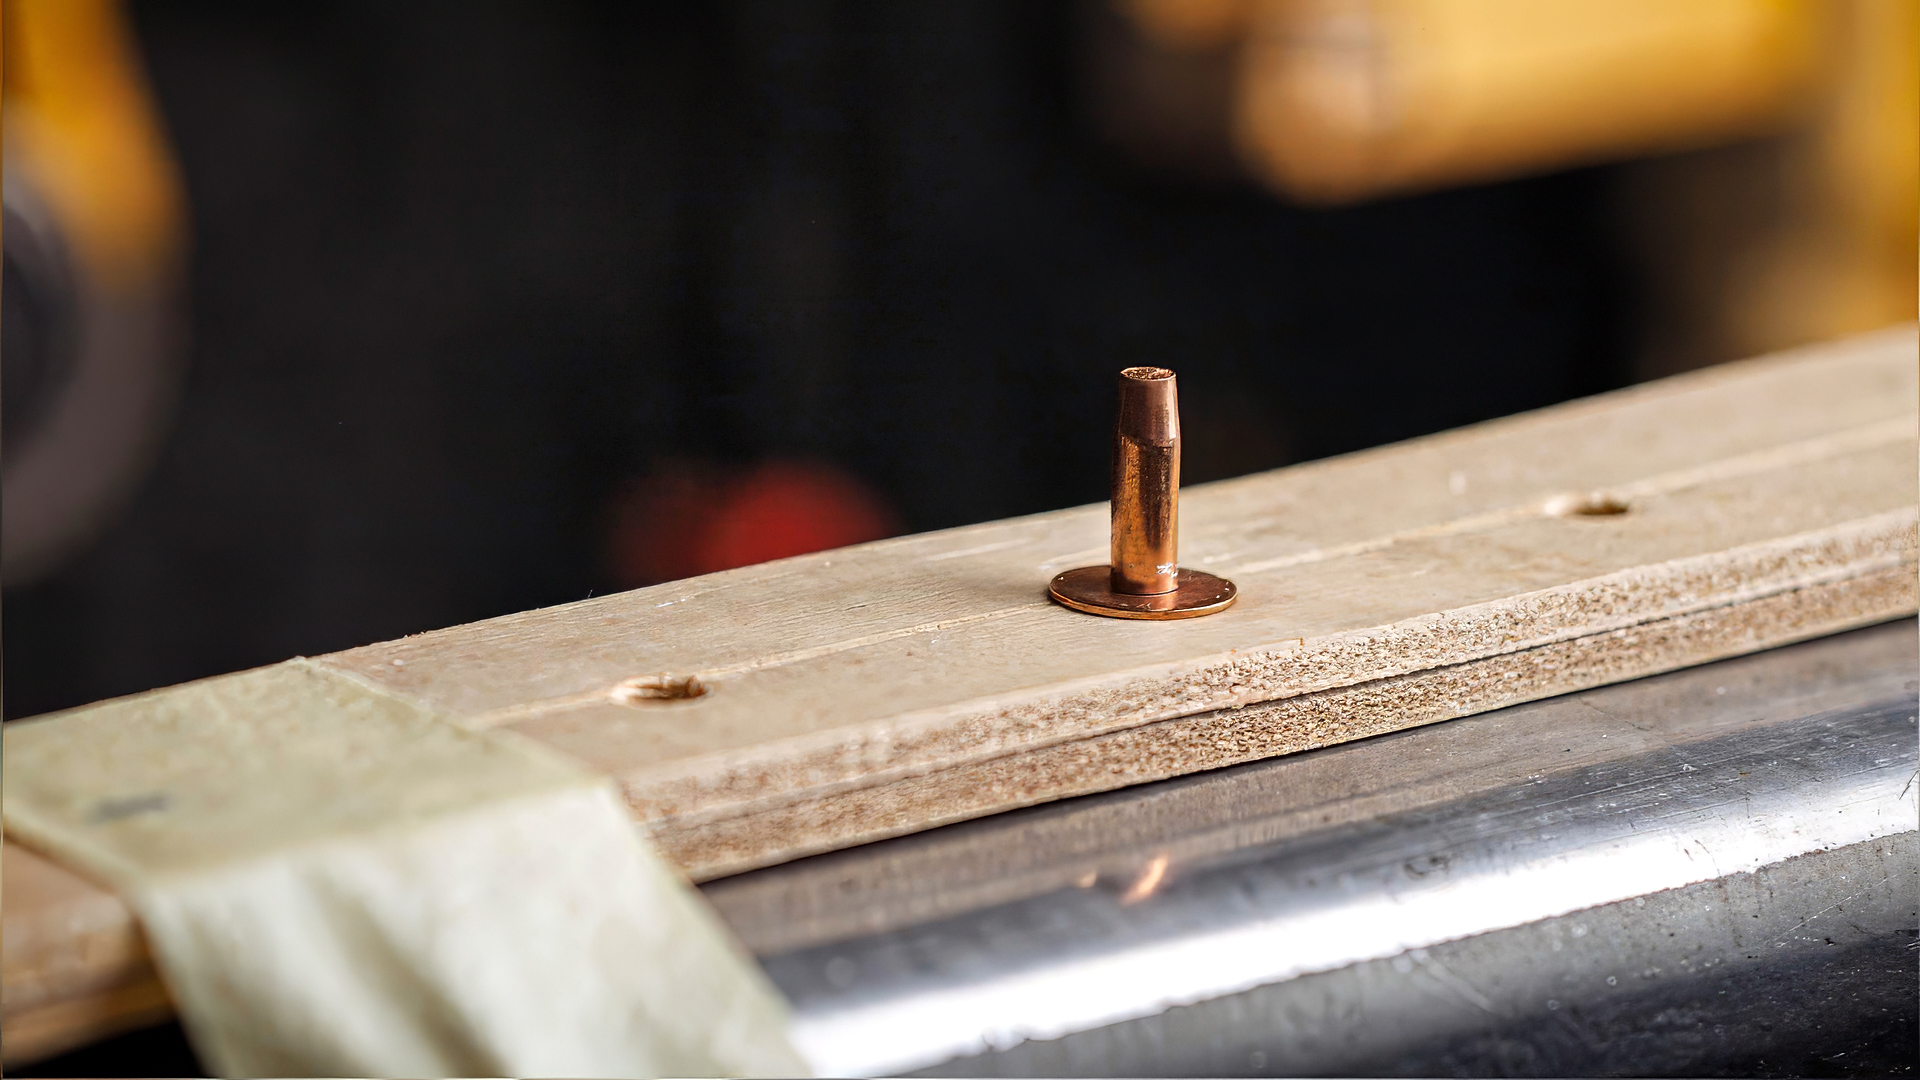
Once the burr is seated, trim the excess shank with end-cutting pliers. The cut-off piece of metal will fly off, so hold a piece of cloth over the shank while you cut and wear safety glasses. Leave just enough metal above the burr to peen it safely into a new rivet head.
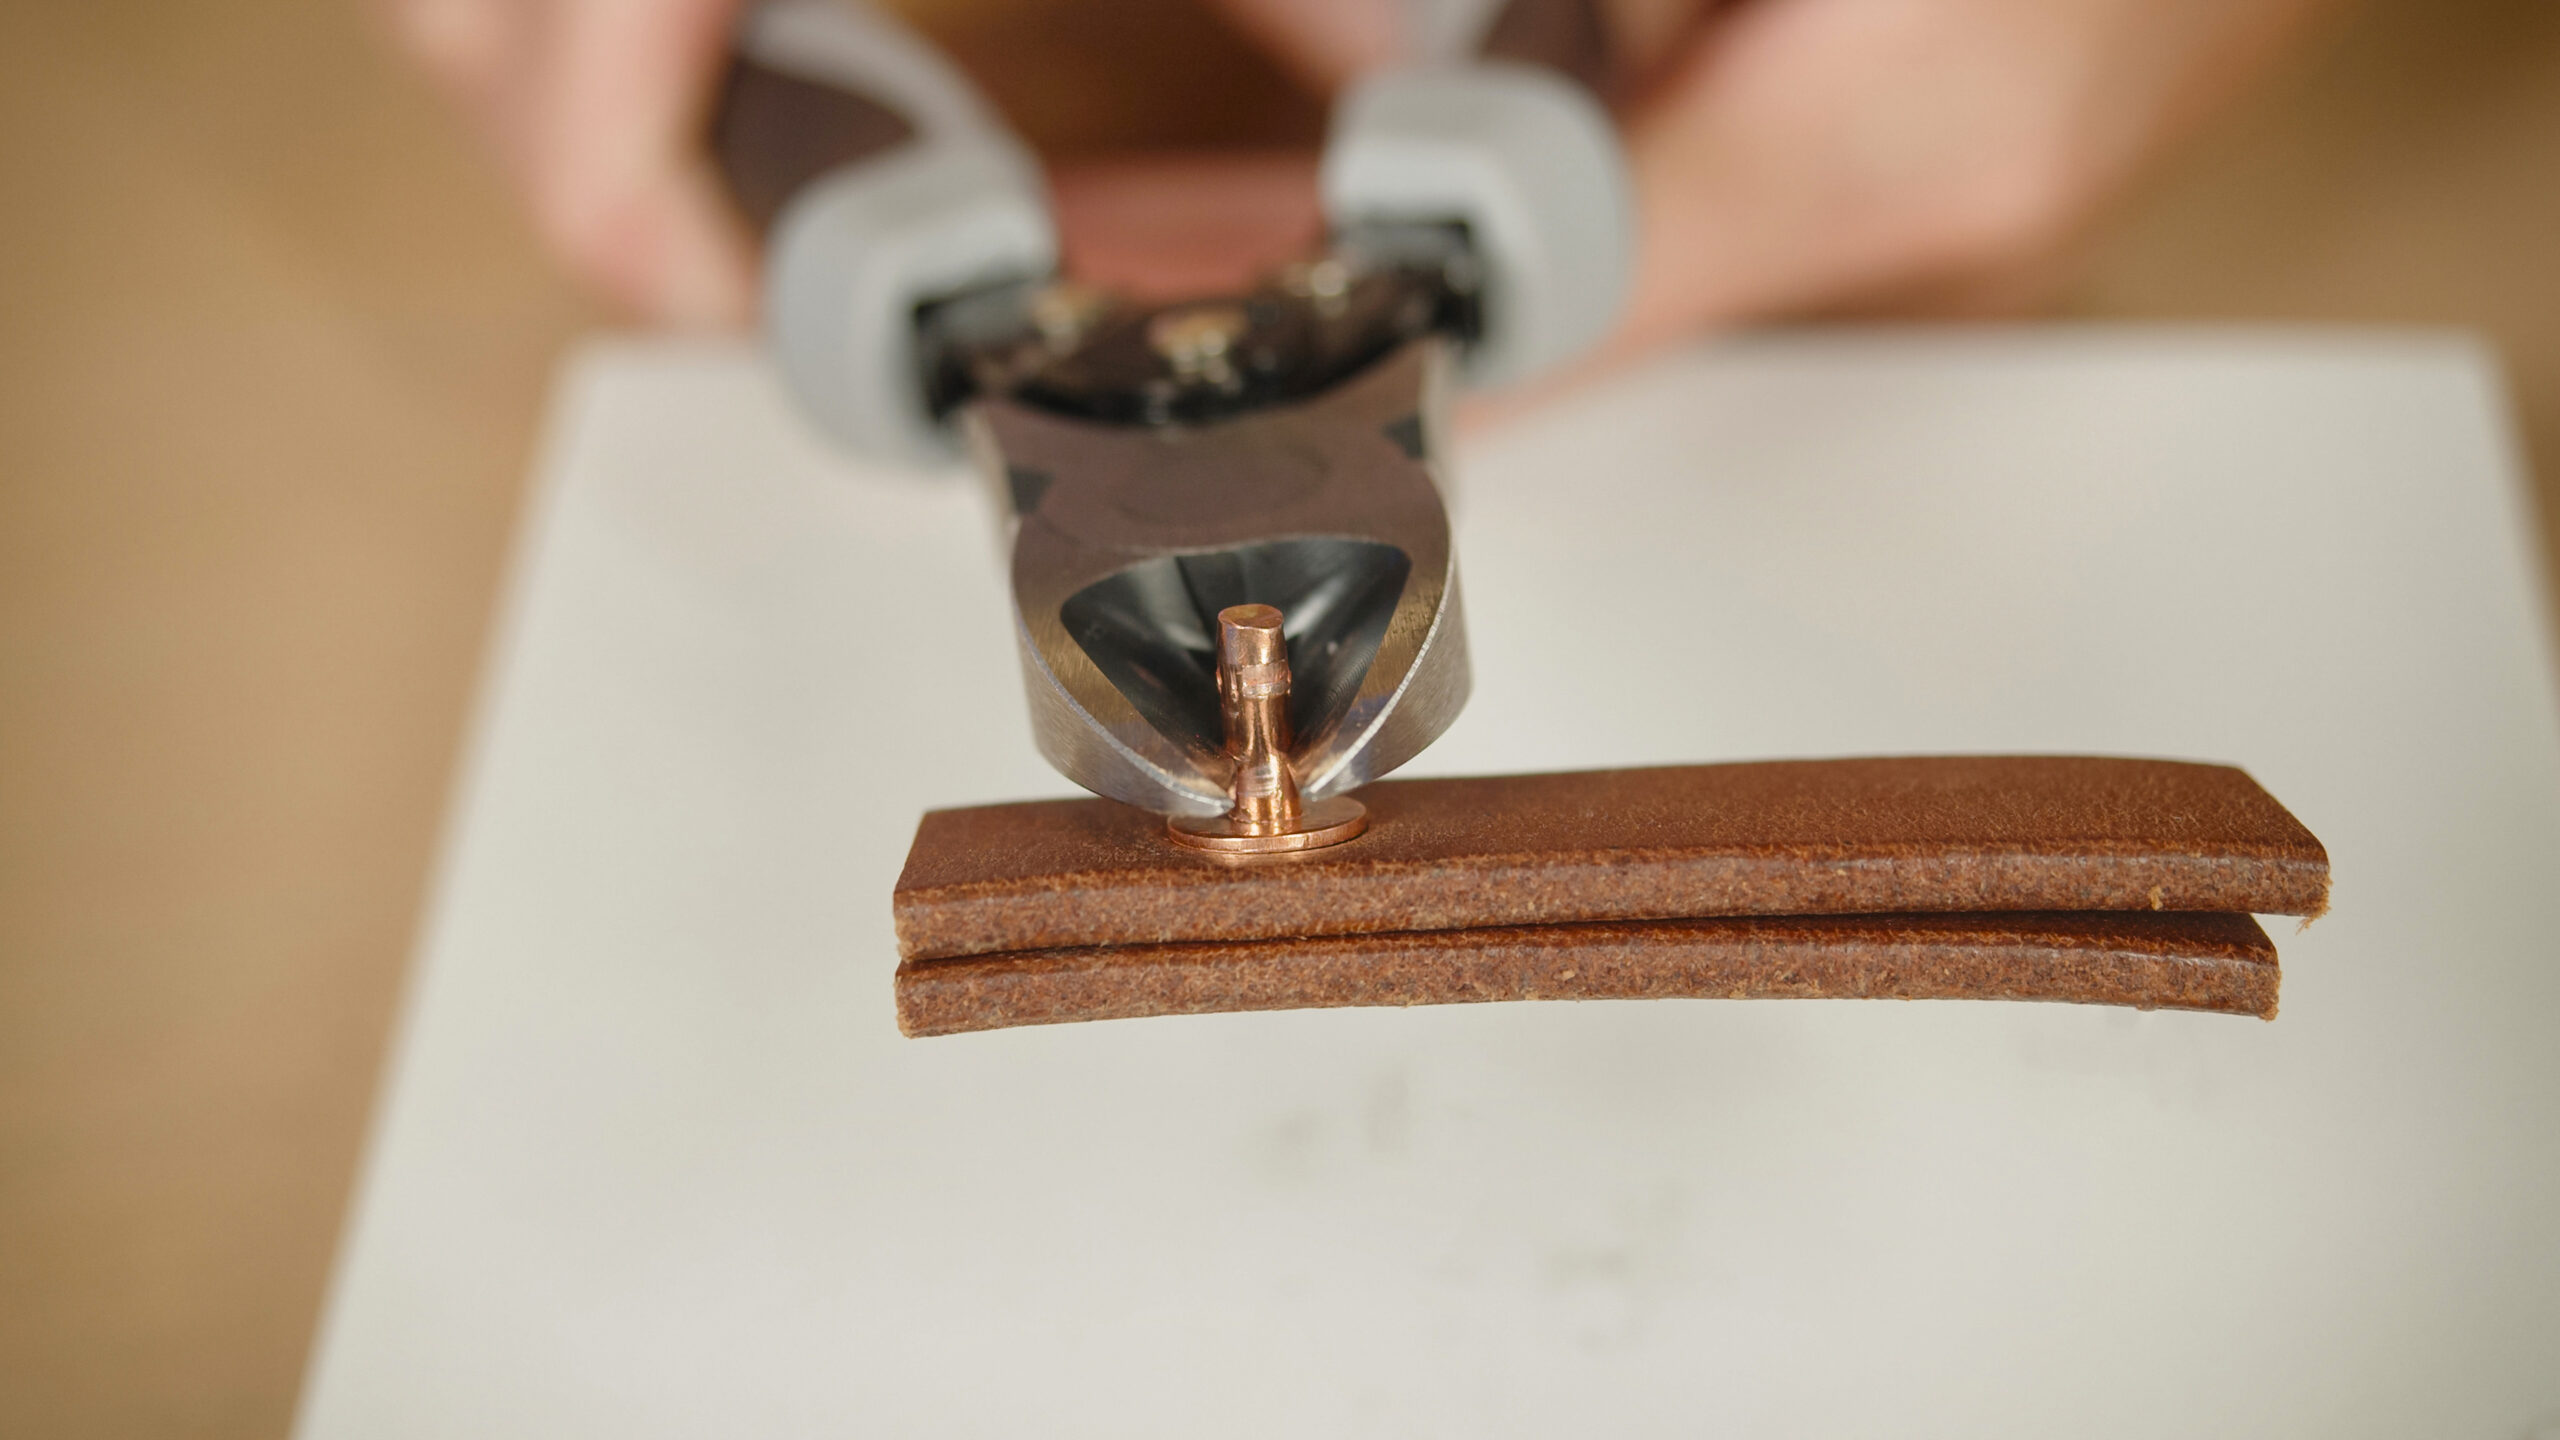
As a rule of thumb, aim for roughly 2 to 4 mm depending on the rivet size. With smaller rivets about 2 mm may be enough; with larger rivets or a more shaped head, you may need a little more.
It helps to cut the shank in two goes. First cut about halfway through the shank, then turn the pliers 90° and finish the cut. This leaves a bevel that is easy to tap down and prepare for setting.
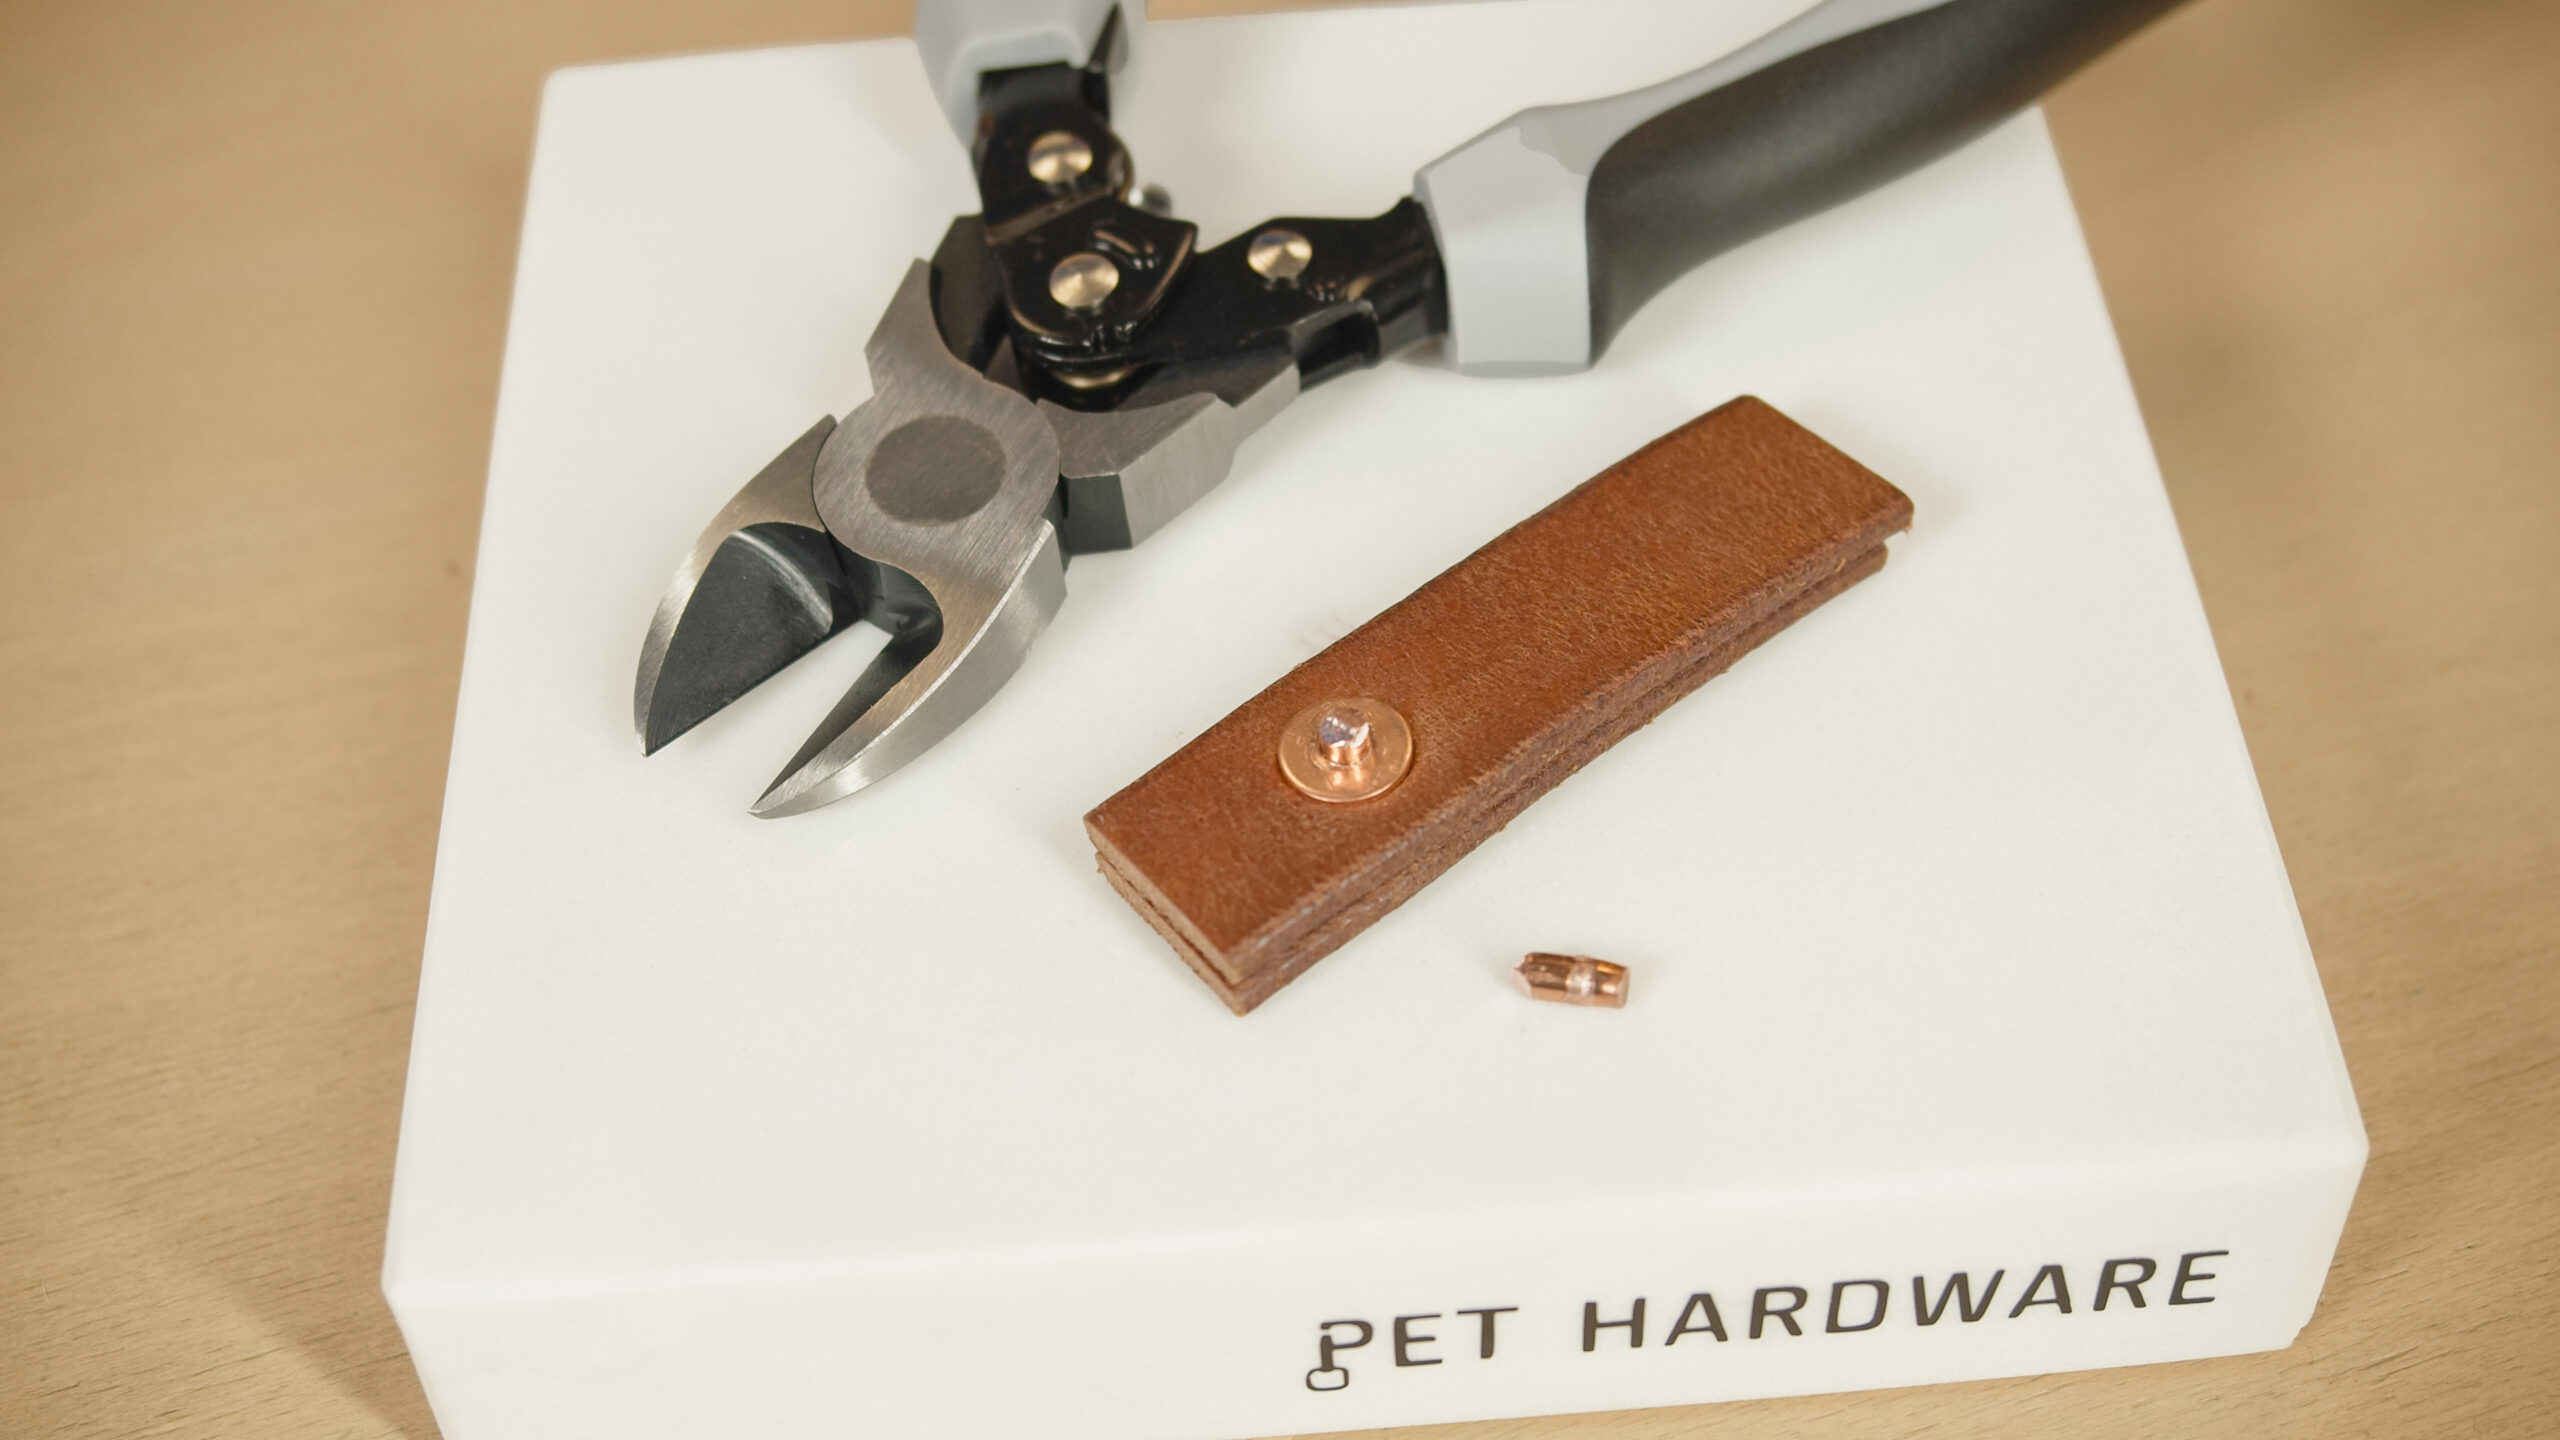
5. Form the rivet head
You can first tap the bevel down lightly with a hammer. Then use the other part of the setter, the cupped recess meant for forming the head.
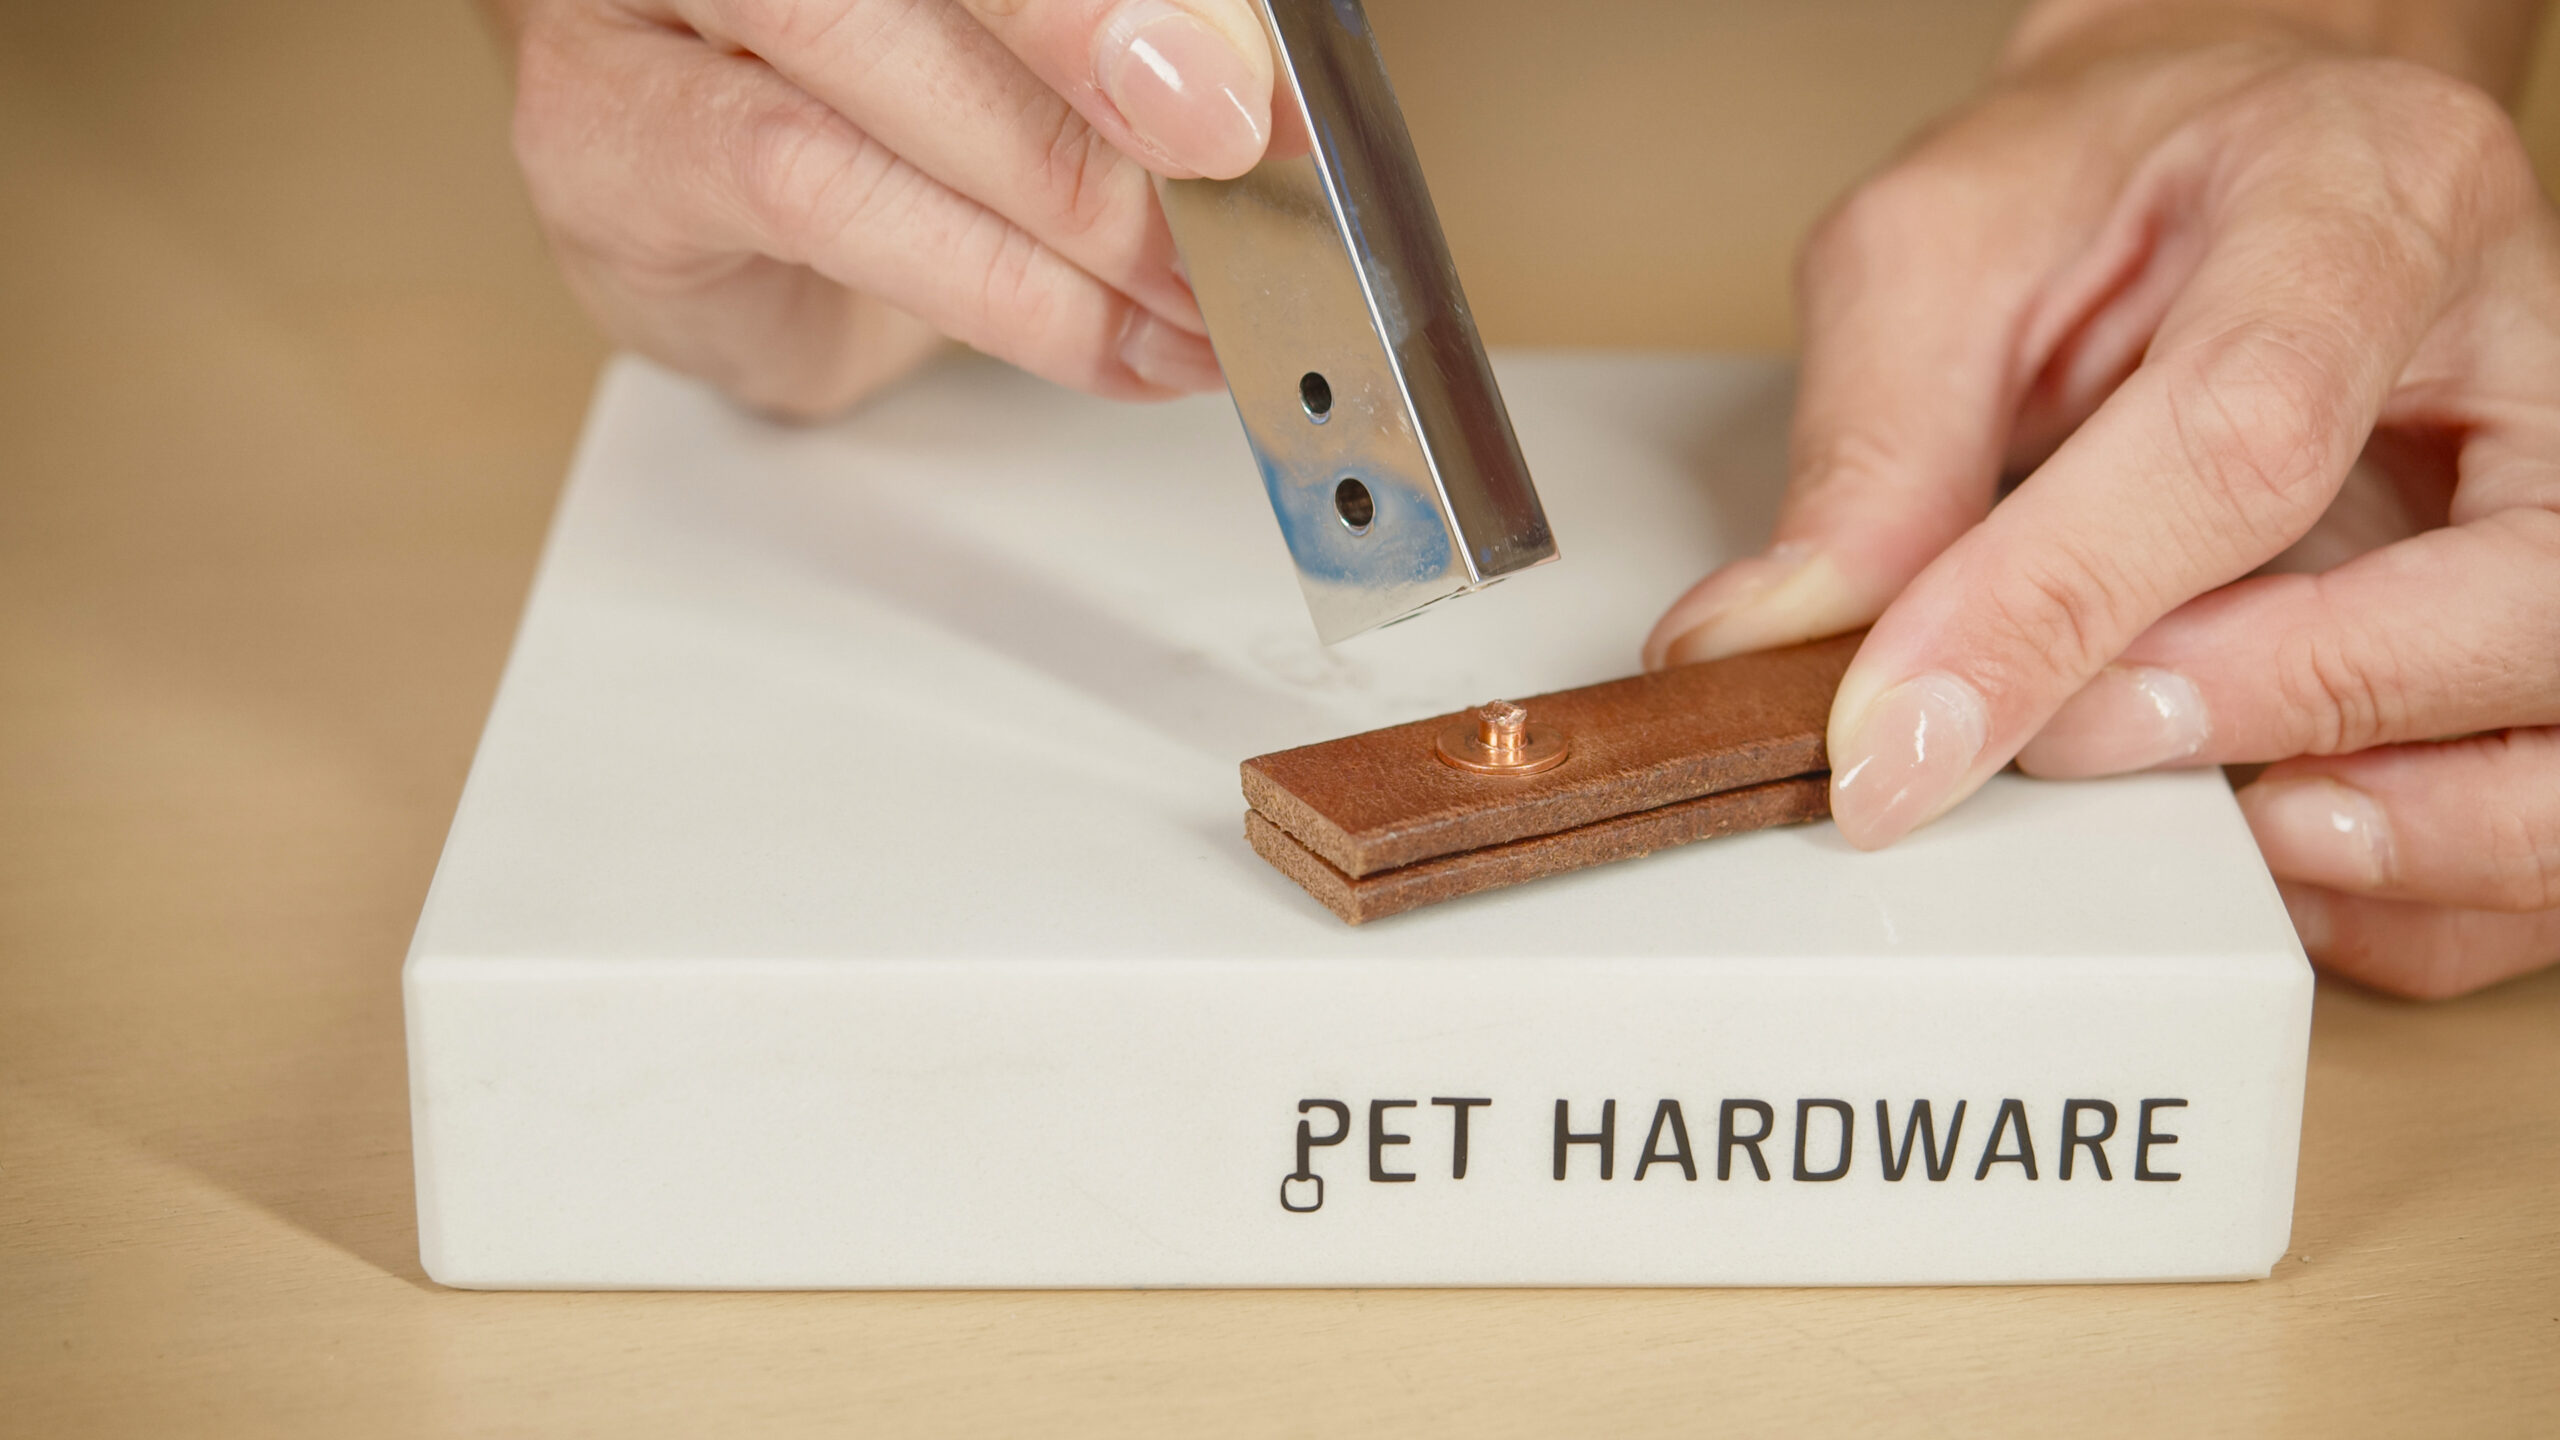
Form the final rivet head with several lighter blows and a slight circular motion. There is no need for a lot of force. Shaping it gradually matters more.
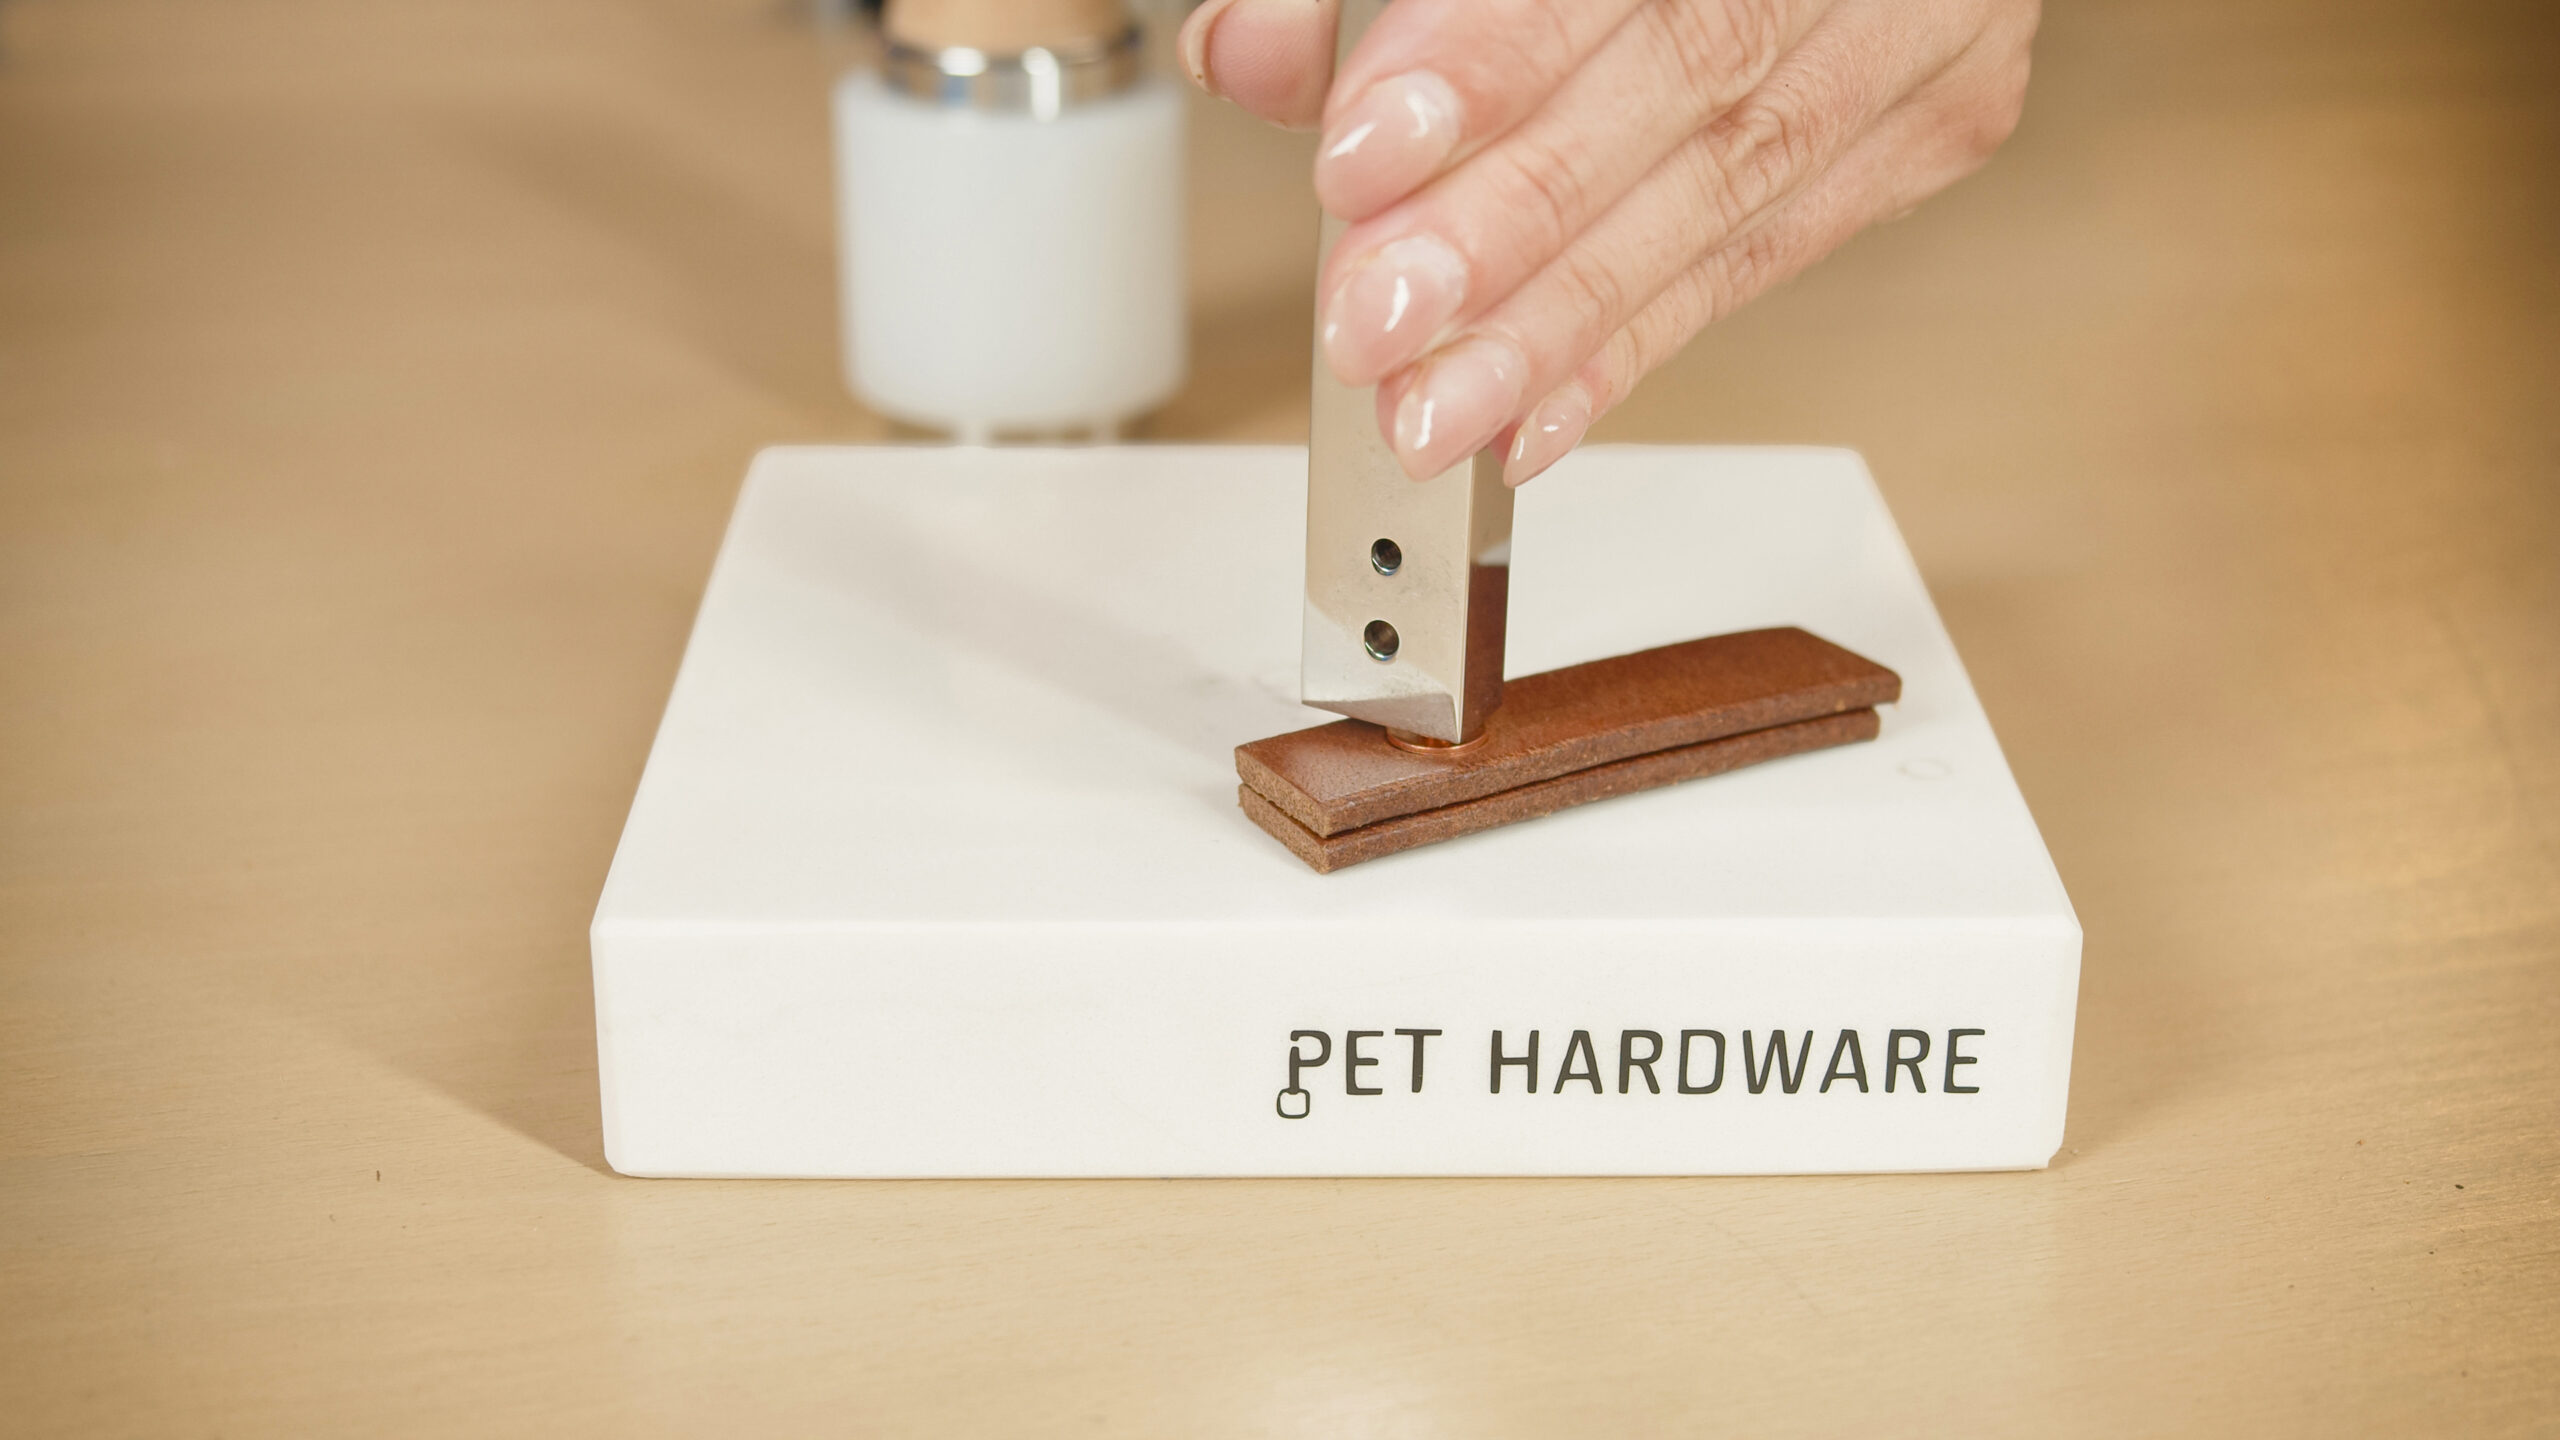
6. Check the finished rivet
Finally, run your finger over the finished rivet. There should be no sharp edge left that could scratch skin, damage leather, snag fabric or tear any other material.
Ways to finish the rivet head
With copper and brass rivets and burrs, you can also influence the look of the newly formed head. It depends on the tools you use and the result that suits the piece.
A clean finish with the rivet setter
The most common option is to finish the head with the setter. After seating the burr and trimming the shank, you use the cupped recess of the setter and form a smoother, more even rivet head with gradual, lighter blows.
This option suits pieces where you want a clean, controlled finish. You use the setter and anvil the same way as with ordinary rivets; see How to set rivets by hand.
A rustic finish with a peening hammer
If you want a more pronounced handmade look, you can work the finished rivet head a little more by tapping it with a hammer. A small ball-peen hammer, for example, leaves a more irregular texture on the metal.
You can get a similar effect with another suitable hammer. What matters most is the shape of the hammer face and the mark it leaves on the metal. Work gradually with lighter blows and finally check that no sharp edge is left on the rivet.
Peening with a flat hammer
Another option is to skip the setter after trimming the shank and peen the rivet directly with a flat-faced hammer. The head will look different from one formed with a setter, which can suit pieces where you want the handwork to show.
With this option, work carefully so the rivet head spreads evenly and no sharp rims form on it.
Whichever option you choose, check the finished rivet head with your finger at the end. It should have no sharp edge or burr that could damage the material or feel unpleasant in use.
Practical riveting tips
When you work with copper and brass rivets and burrs, a few simple aids make the job easier and help you get a cleaner result.
A spacer to protect the burr and mark the length
When trimming the shank, you can use a piece of paper or another thin material. Slip it over the shank above the burr and use it as a simple aid.
It helps you in two ways:
- it protects the burr from damage while you cut,
- it helps you judge where to trim the shank.
This makes it easier to leave roughly 2 to 4 mm of metal above the burr, depending on the rivet size and the head finish you want.
Backing thinner materials
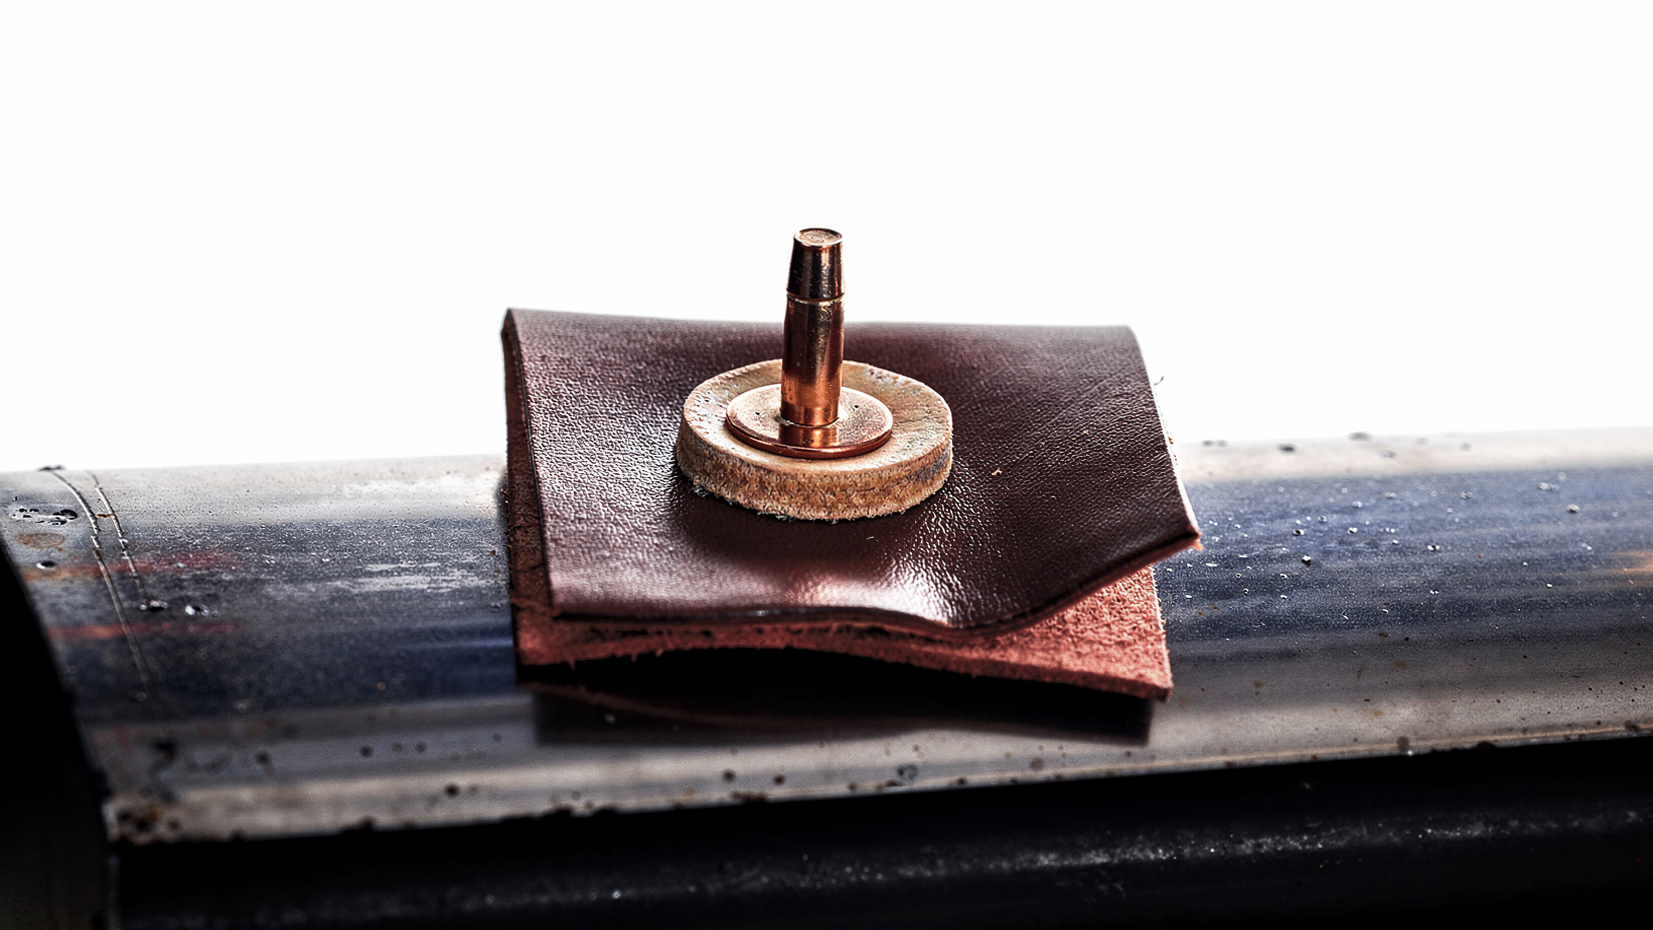
If you are riveting thinner material, such as thin leather or fabric, a piece of thicker leather can help. Slip it over the shank before the copper or brass burr.
This extra leather washer spreads the pressure and comes in handy mainly with materials that could deform or get damaged during riveting.
Polishing the rivet head
You can also improve the look of the finished rivet by polishing it. First sand the rivet head lightly with sandpaper, moving to finer grits until the surface is smoother.
For a higher shine, use polishing compound. Apply it to a piece of natural leather and gently polish the rivet head. This step is not needed for the joint to work, but it comes in handy where you want the rivet to look cleaner and shinier or to match the overall look of the piece better.
The most common riveting mistakes
With copper and brass rivets and burrs, the key factors are the right shank length, an accurately prepared hole and a careful finish. Most mistakes happen when one of these steps gets rushed.
Watch out above all for:
- a shank that is too short and leaves too little metal to form the head,
- a hole that is too big, so the rivet does not sit tight,
- a burr that stays loose and does not sit down against the material,
- hammer blows that are too hard and can damage the burr or the material,
- a badly cut shank,
- sharp edges on the finished rivet head.
When you are done, always check the rivet not only by eye but with your finger too. The finished joint should be firm, with no play and no sharp edges. If the piece will touch skin, fur or fabric, this check is especially important.
Conclusion
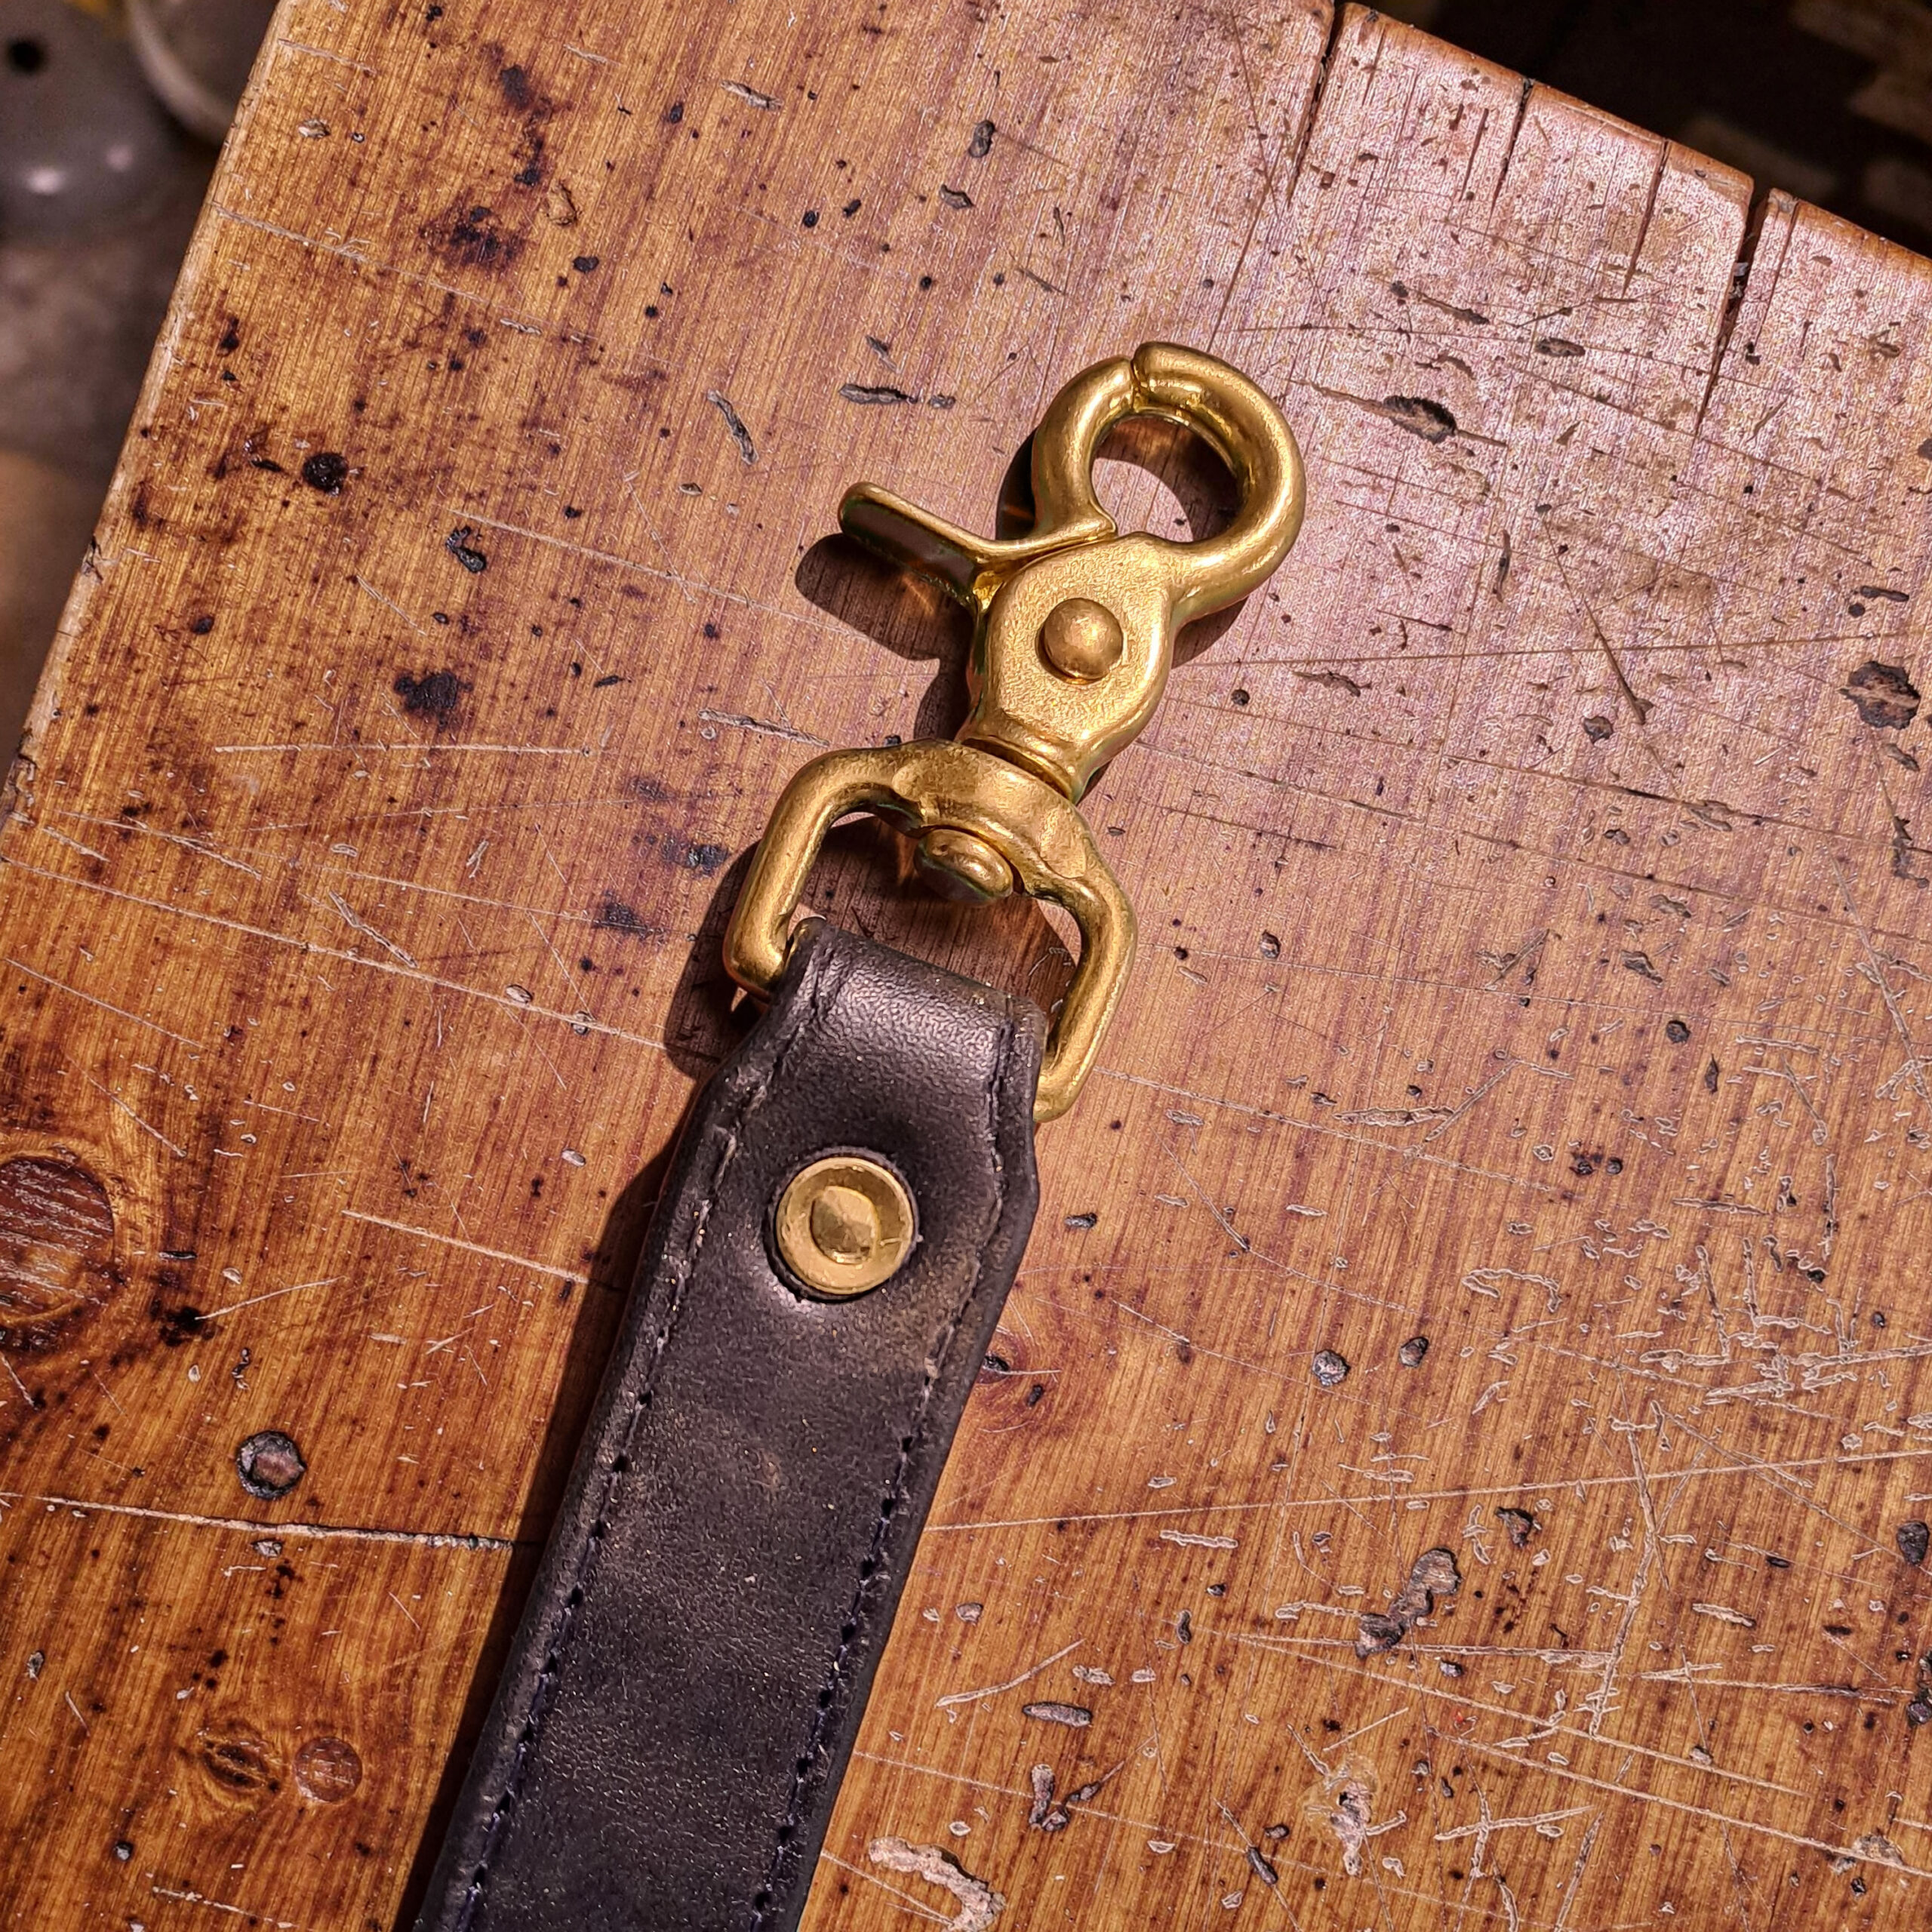
Copper and brass rivets with burrs are not just a practical way to make a strong joint. On the finished piece, they often work as a distinct design element too. A copper or brass head stands out on the finished product, especially on leather.
For the result to look good, though, it pays not to rush. Get the rivet size right, punch a clean hole, seat the burr well and work the head carefully so there are no sharp edges. With this kind of riveting, it is not force that counts but accuracy, patience and the right tools.
When everything comes together, you get a joint that not only holds but also gives the piece a handsome metal detail.
Pethardware.com
The only shop you’ll ever need for crafting collars and leashes.
Visit Pethardware.com